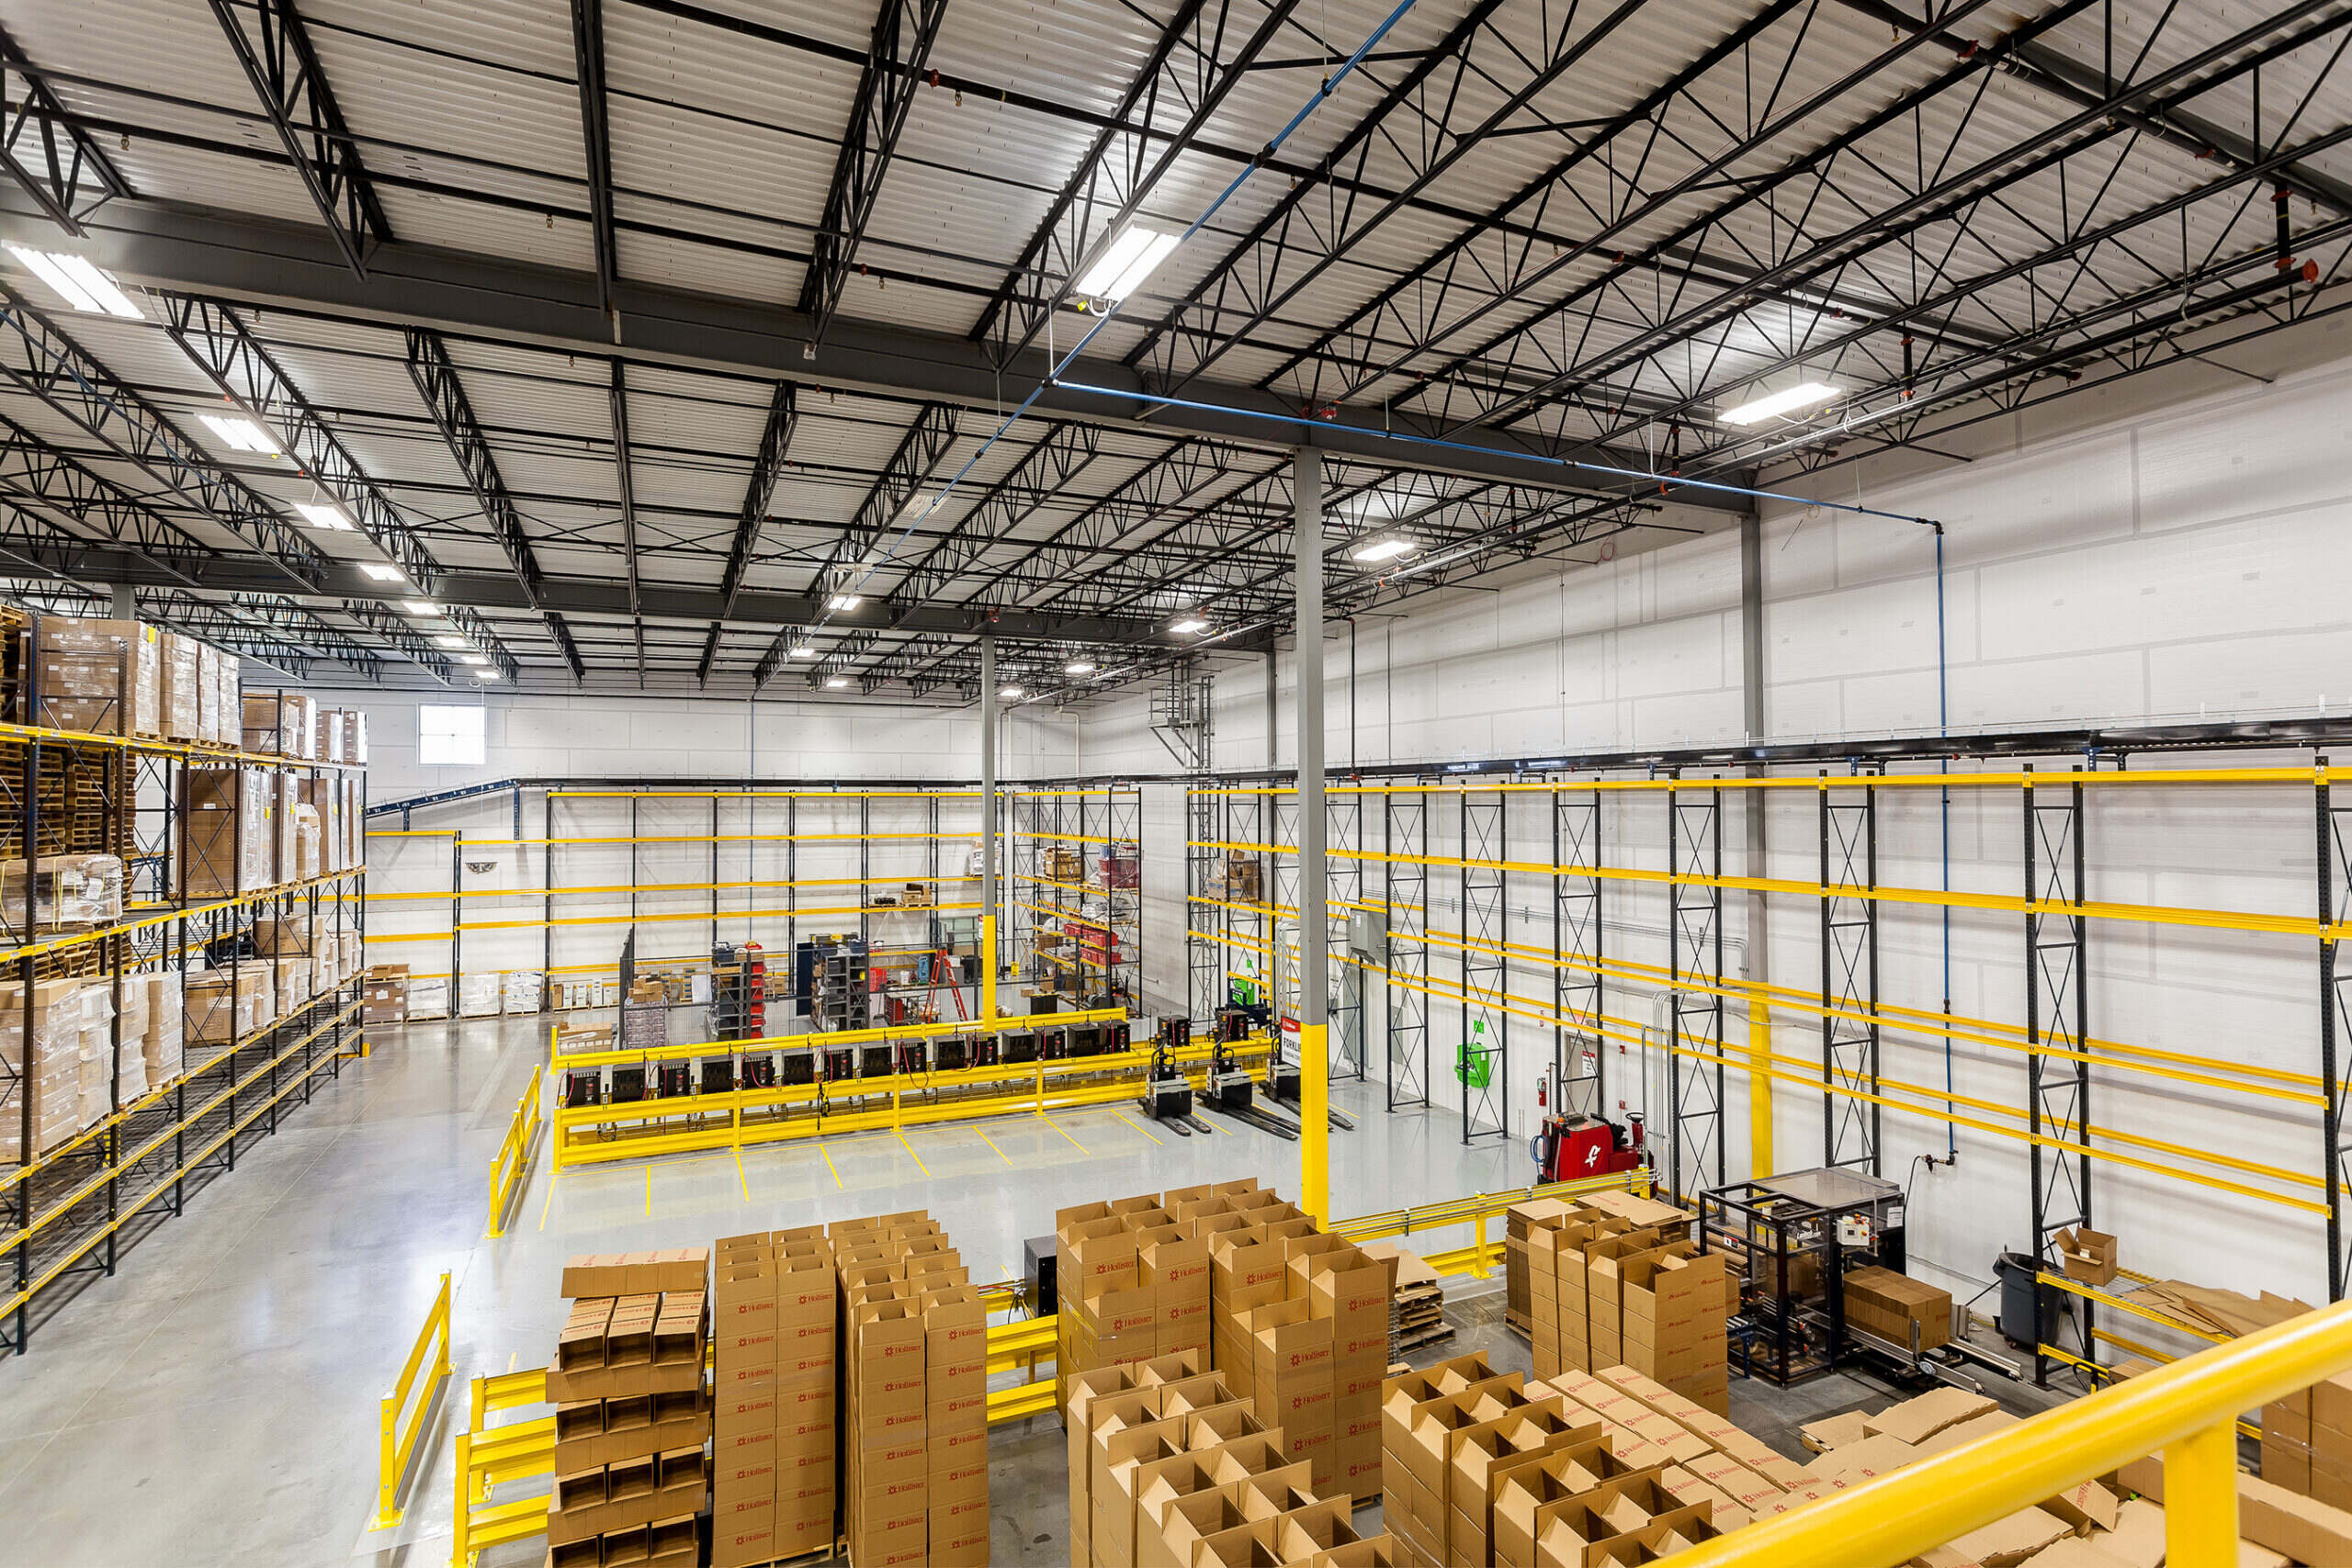
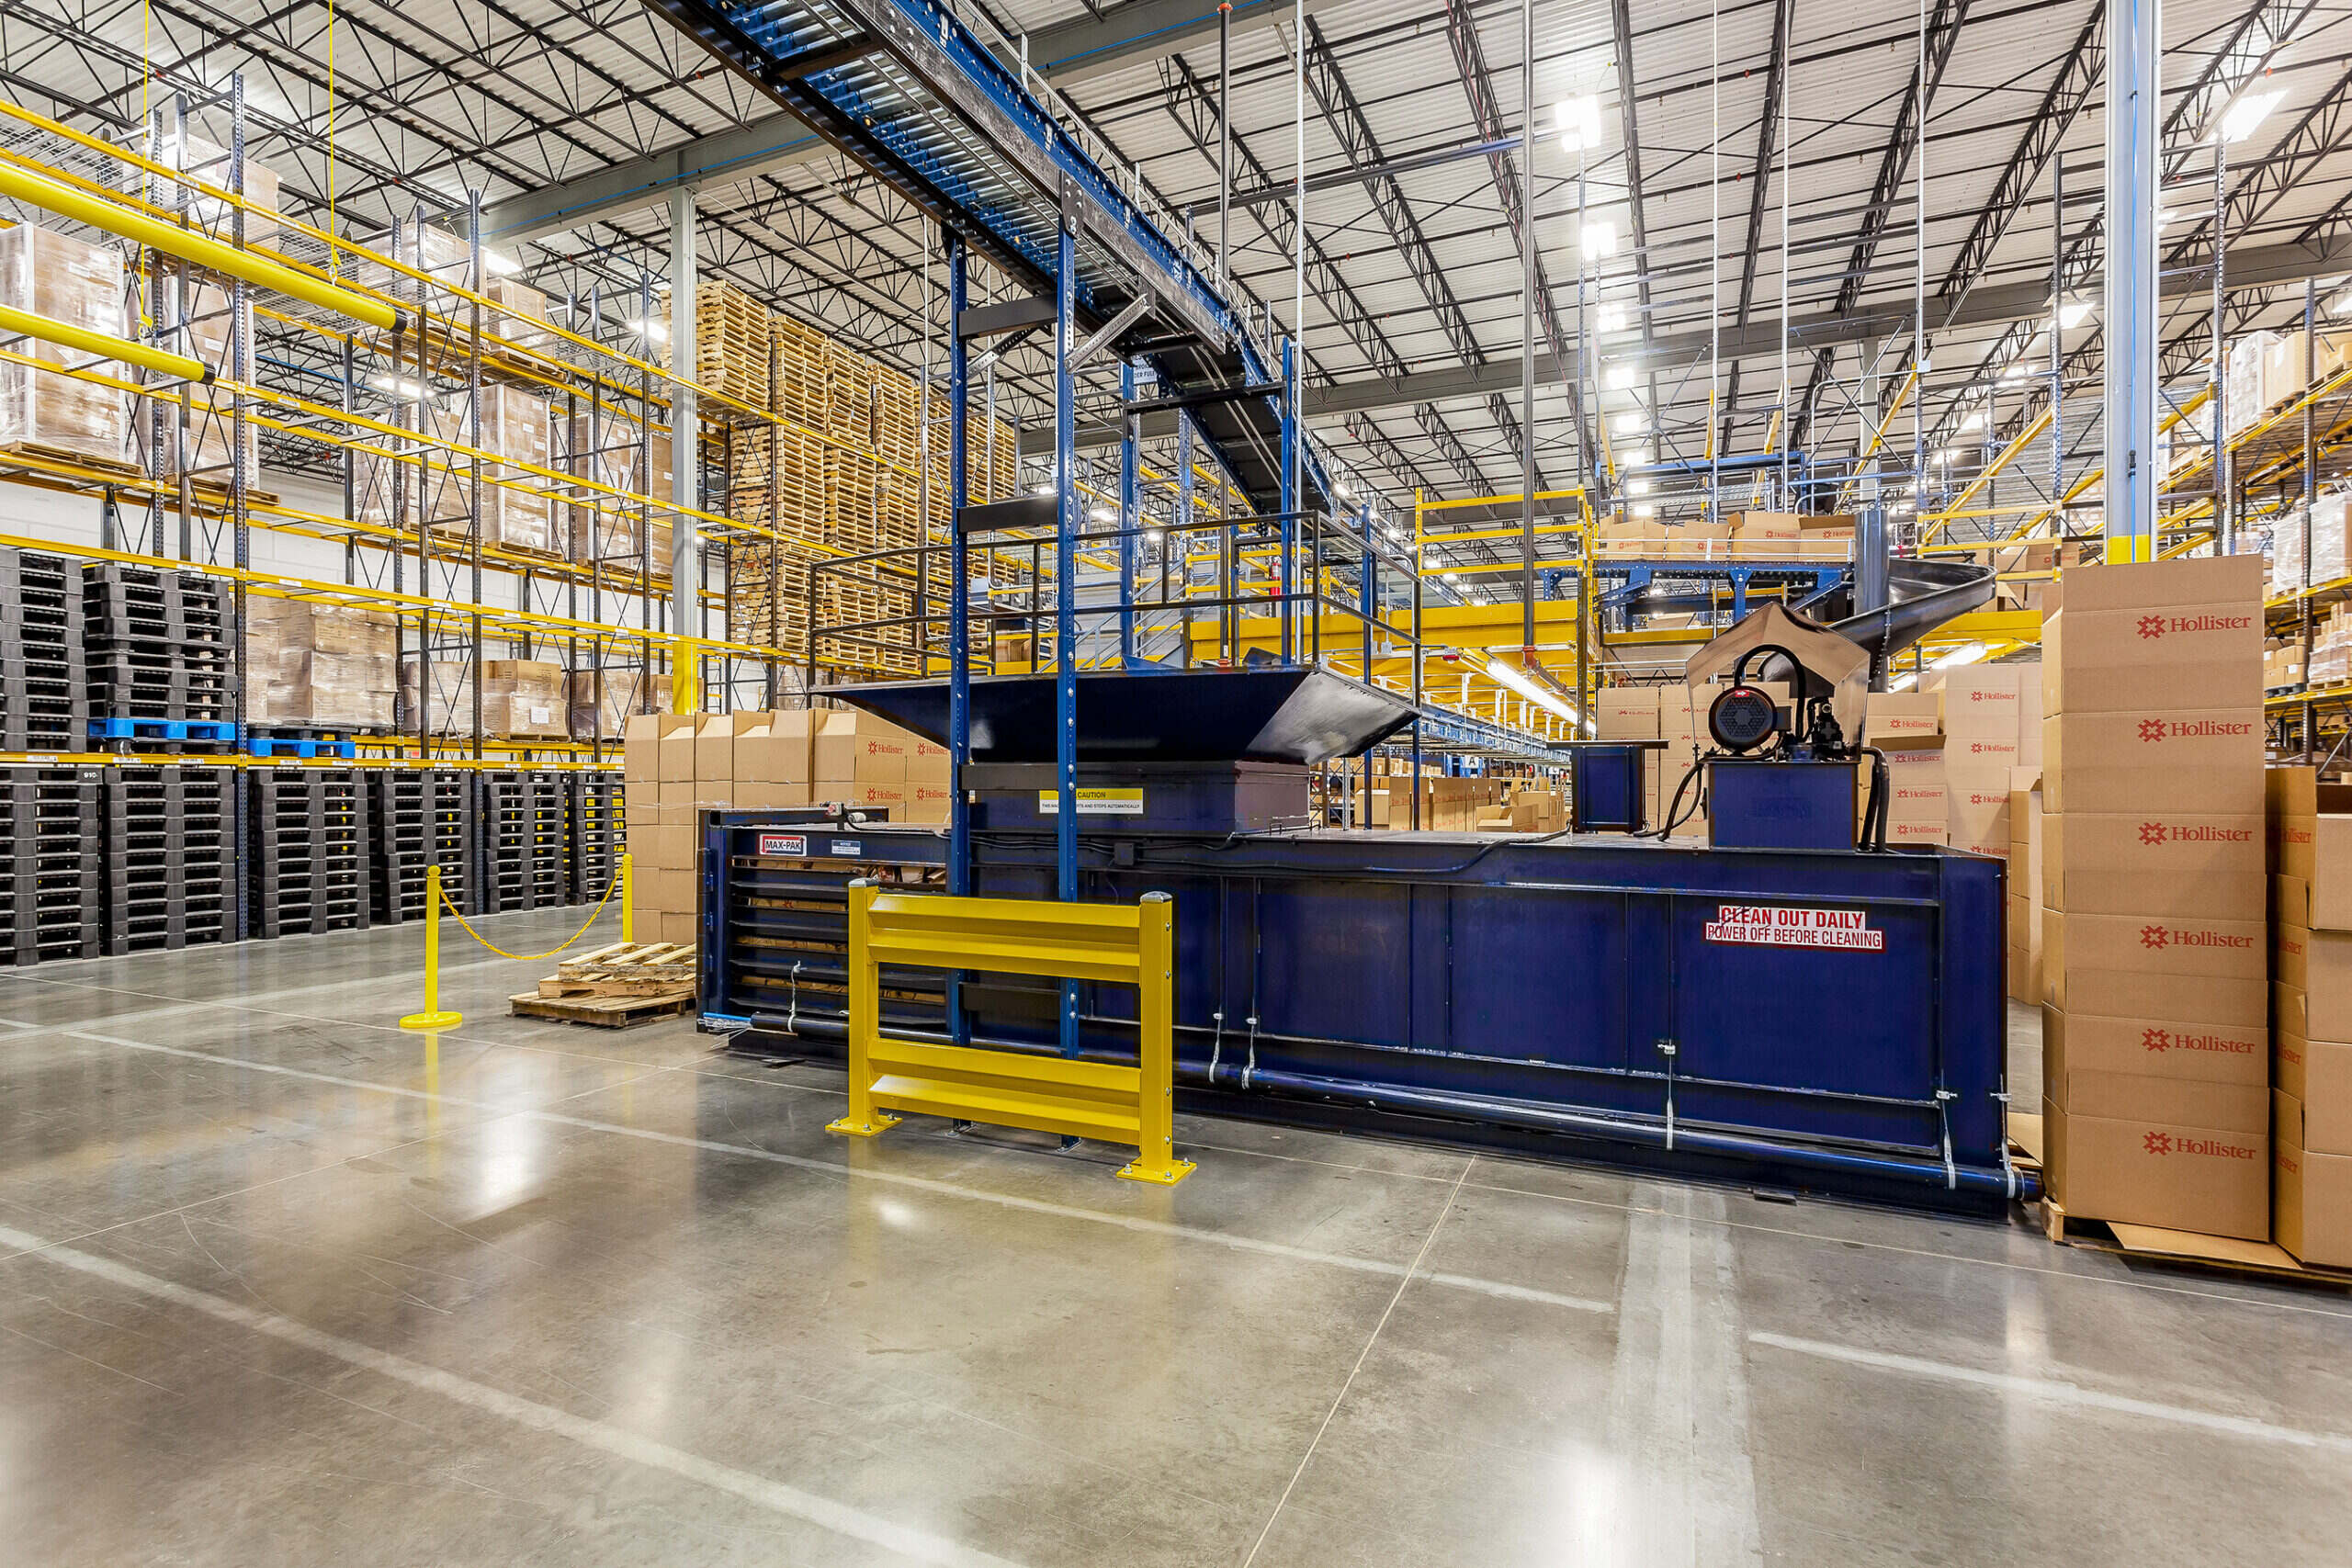
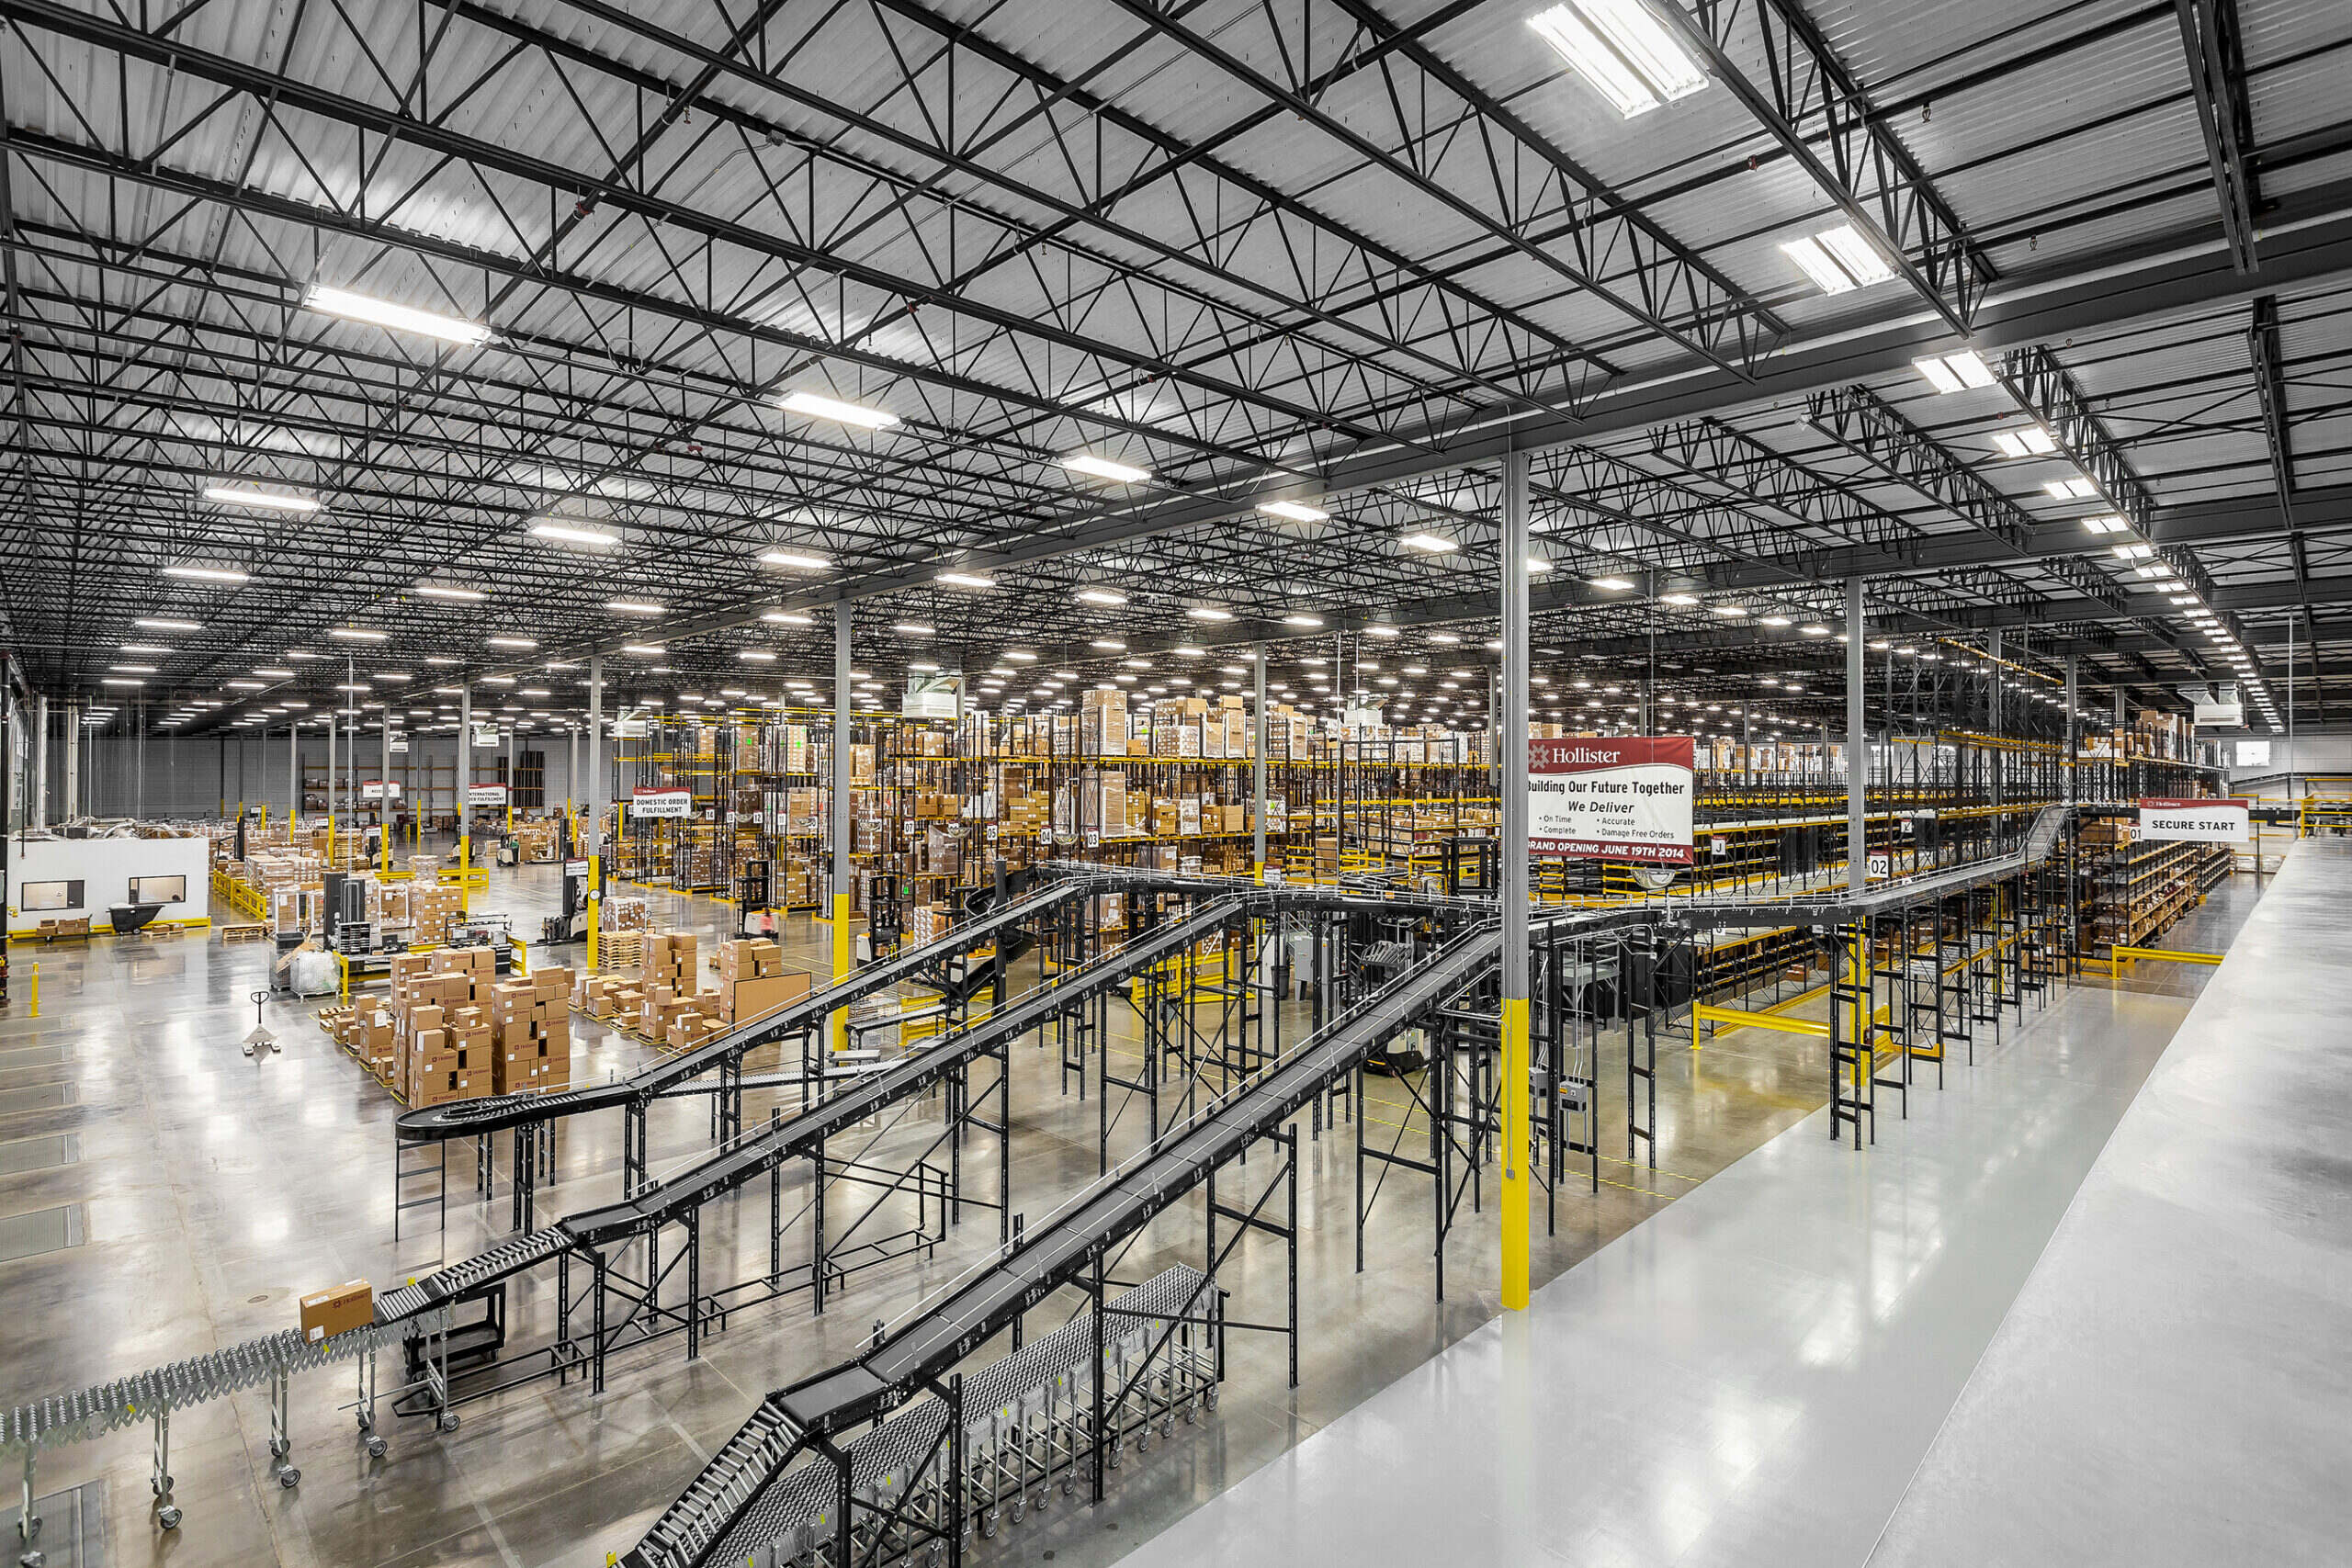
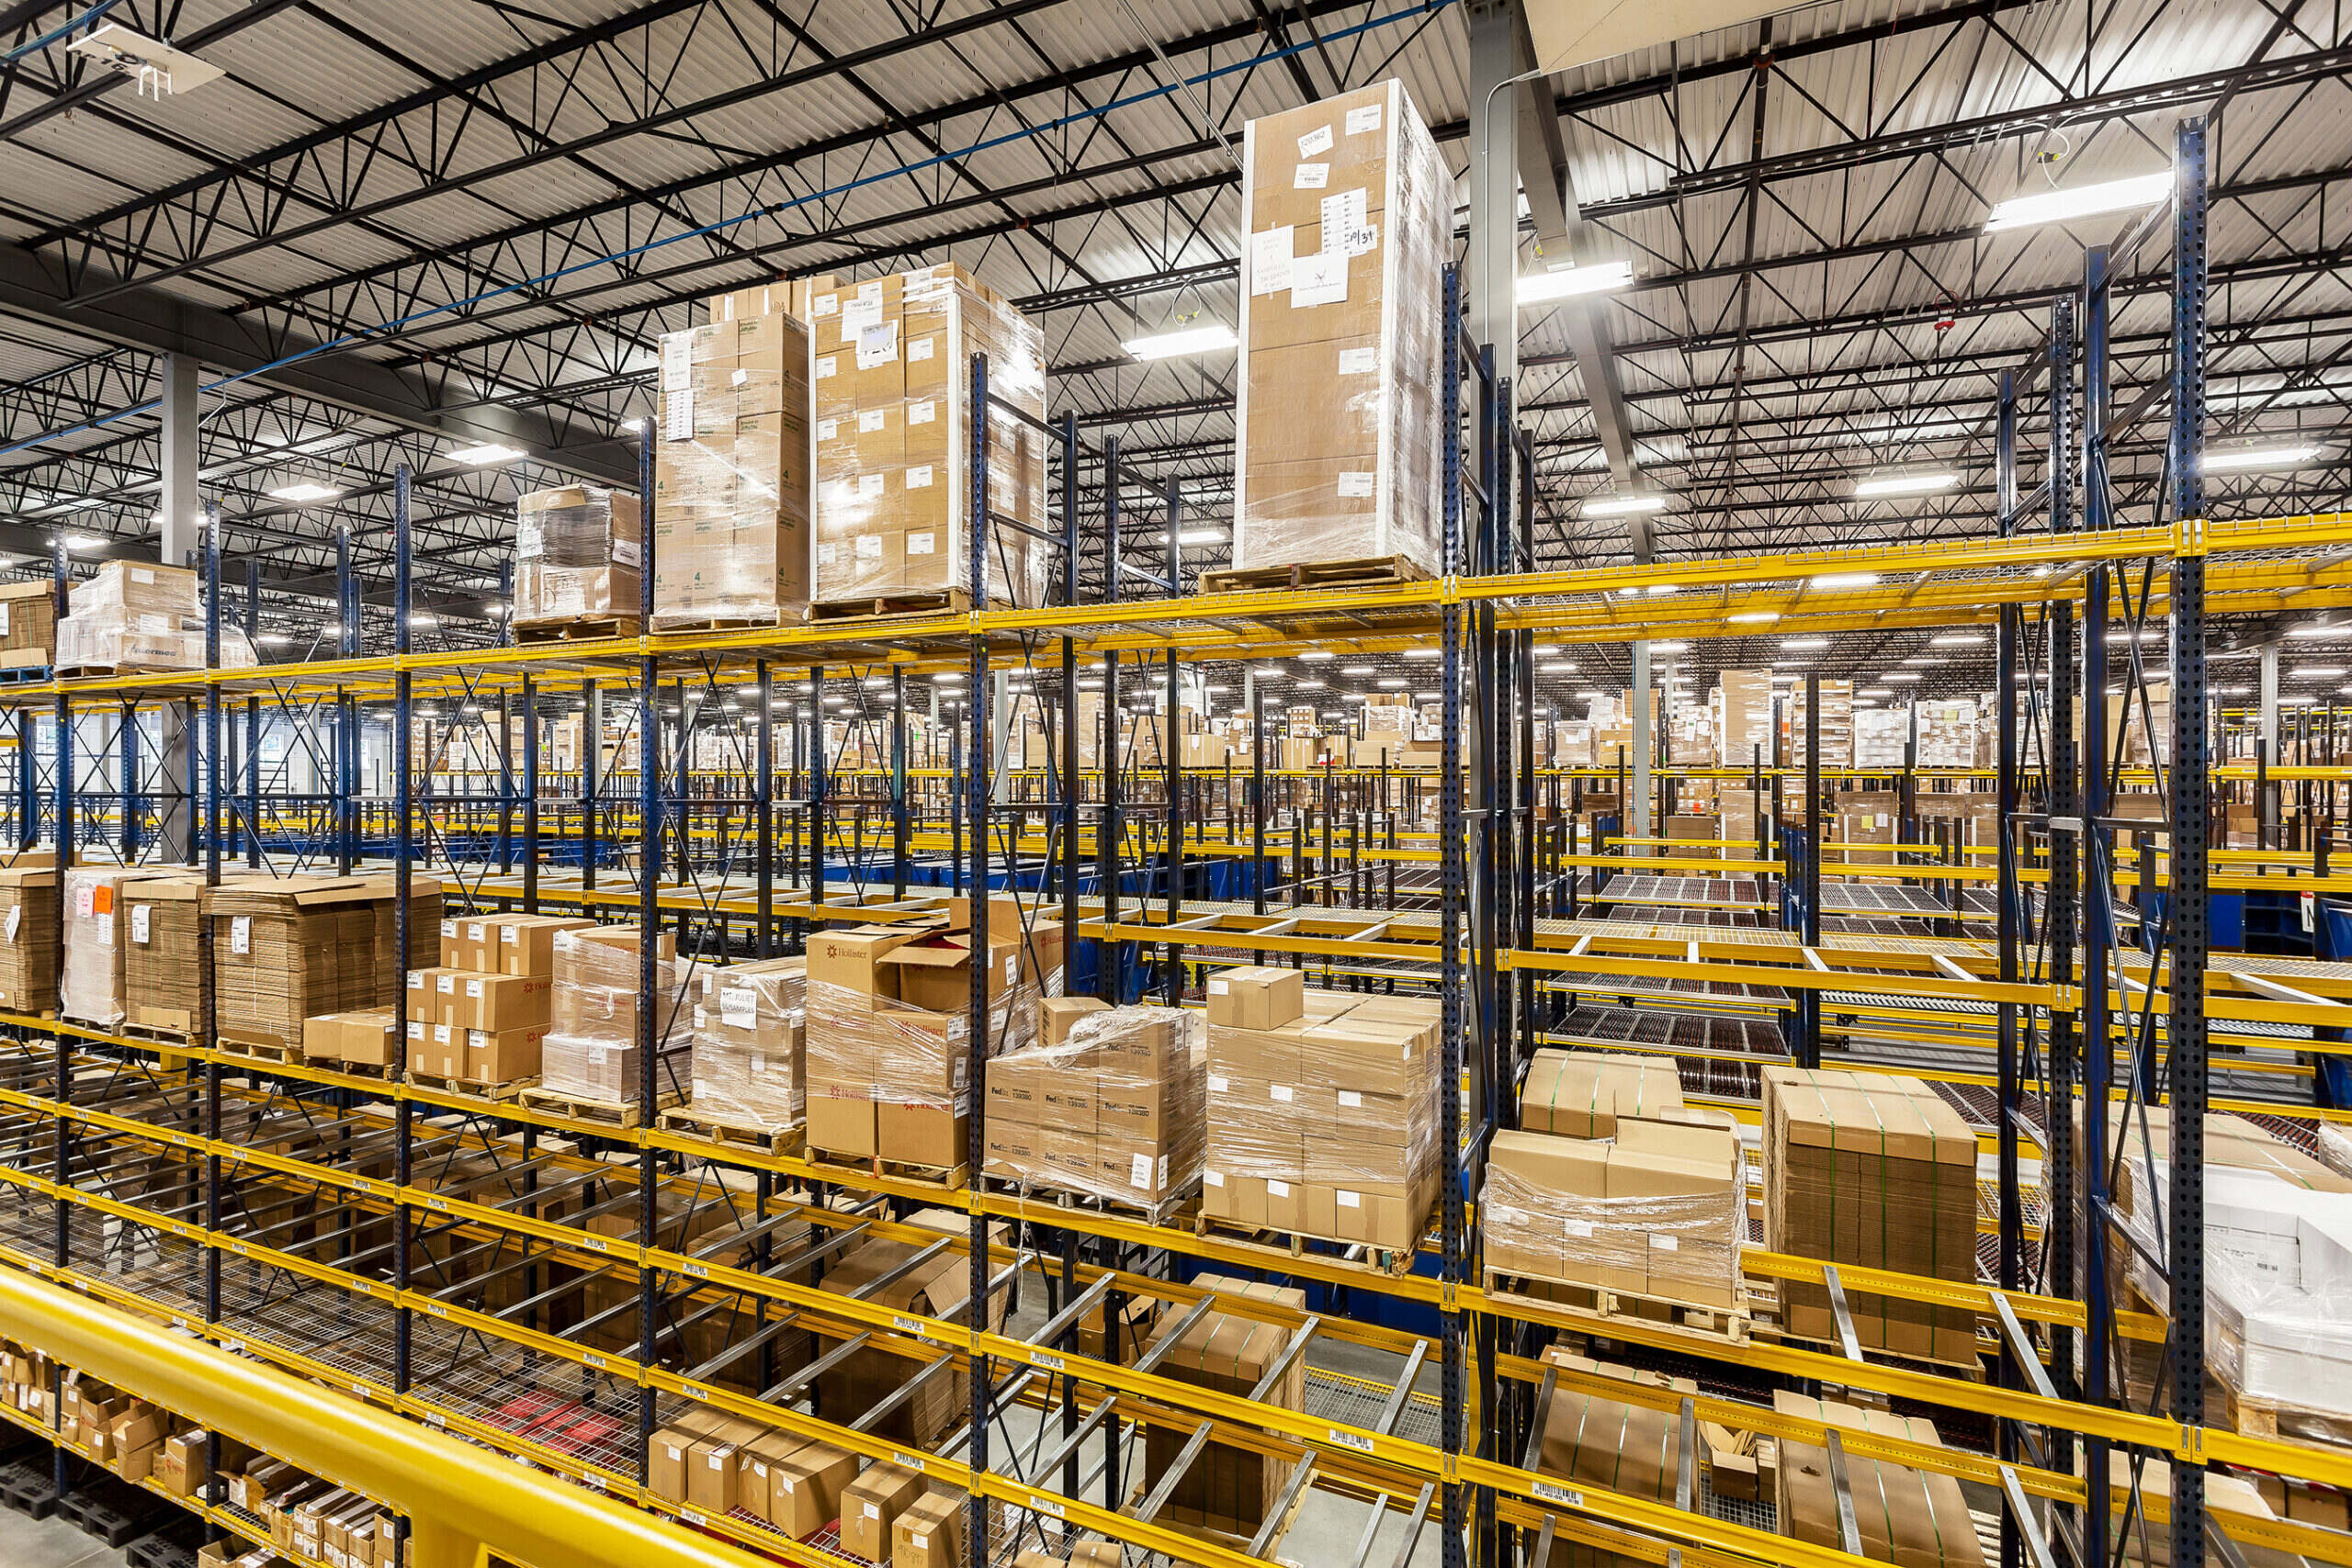
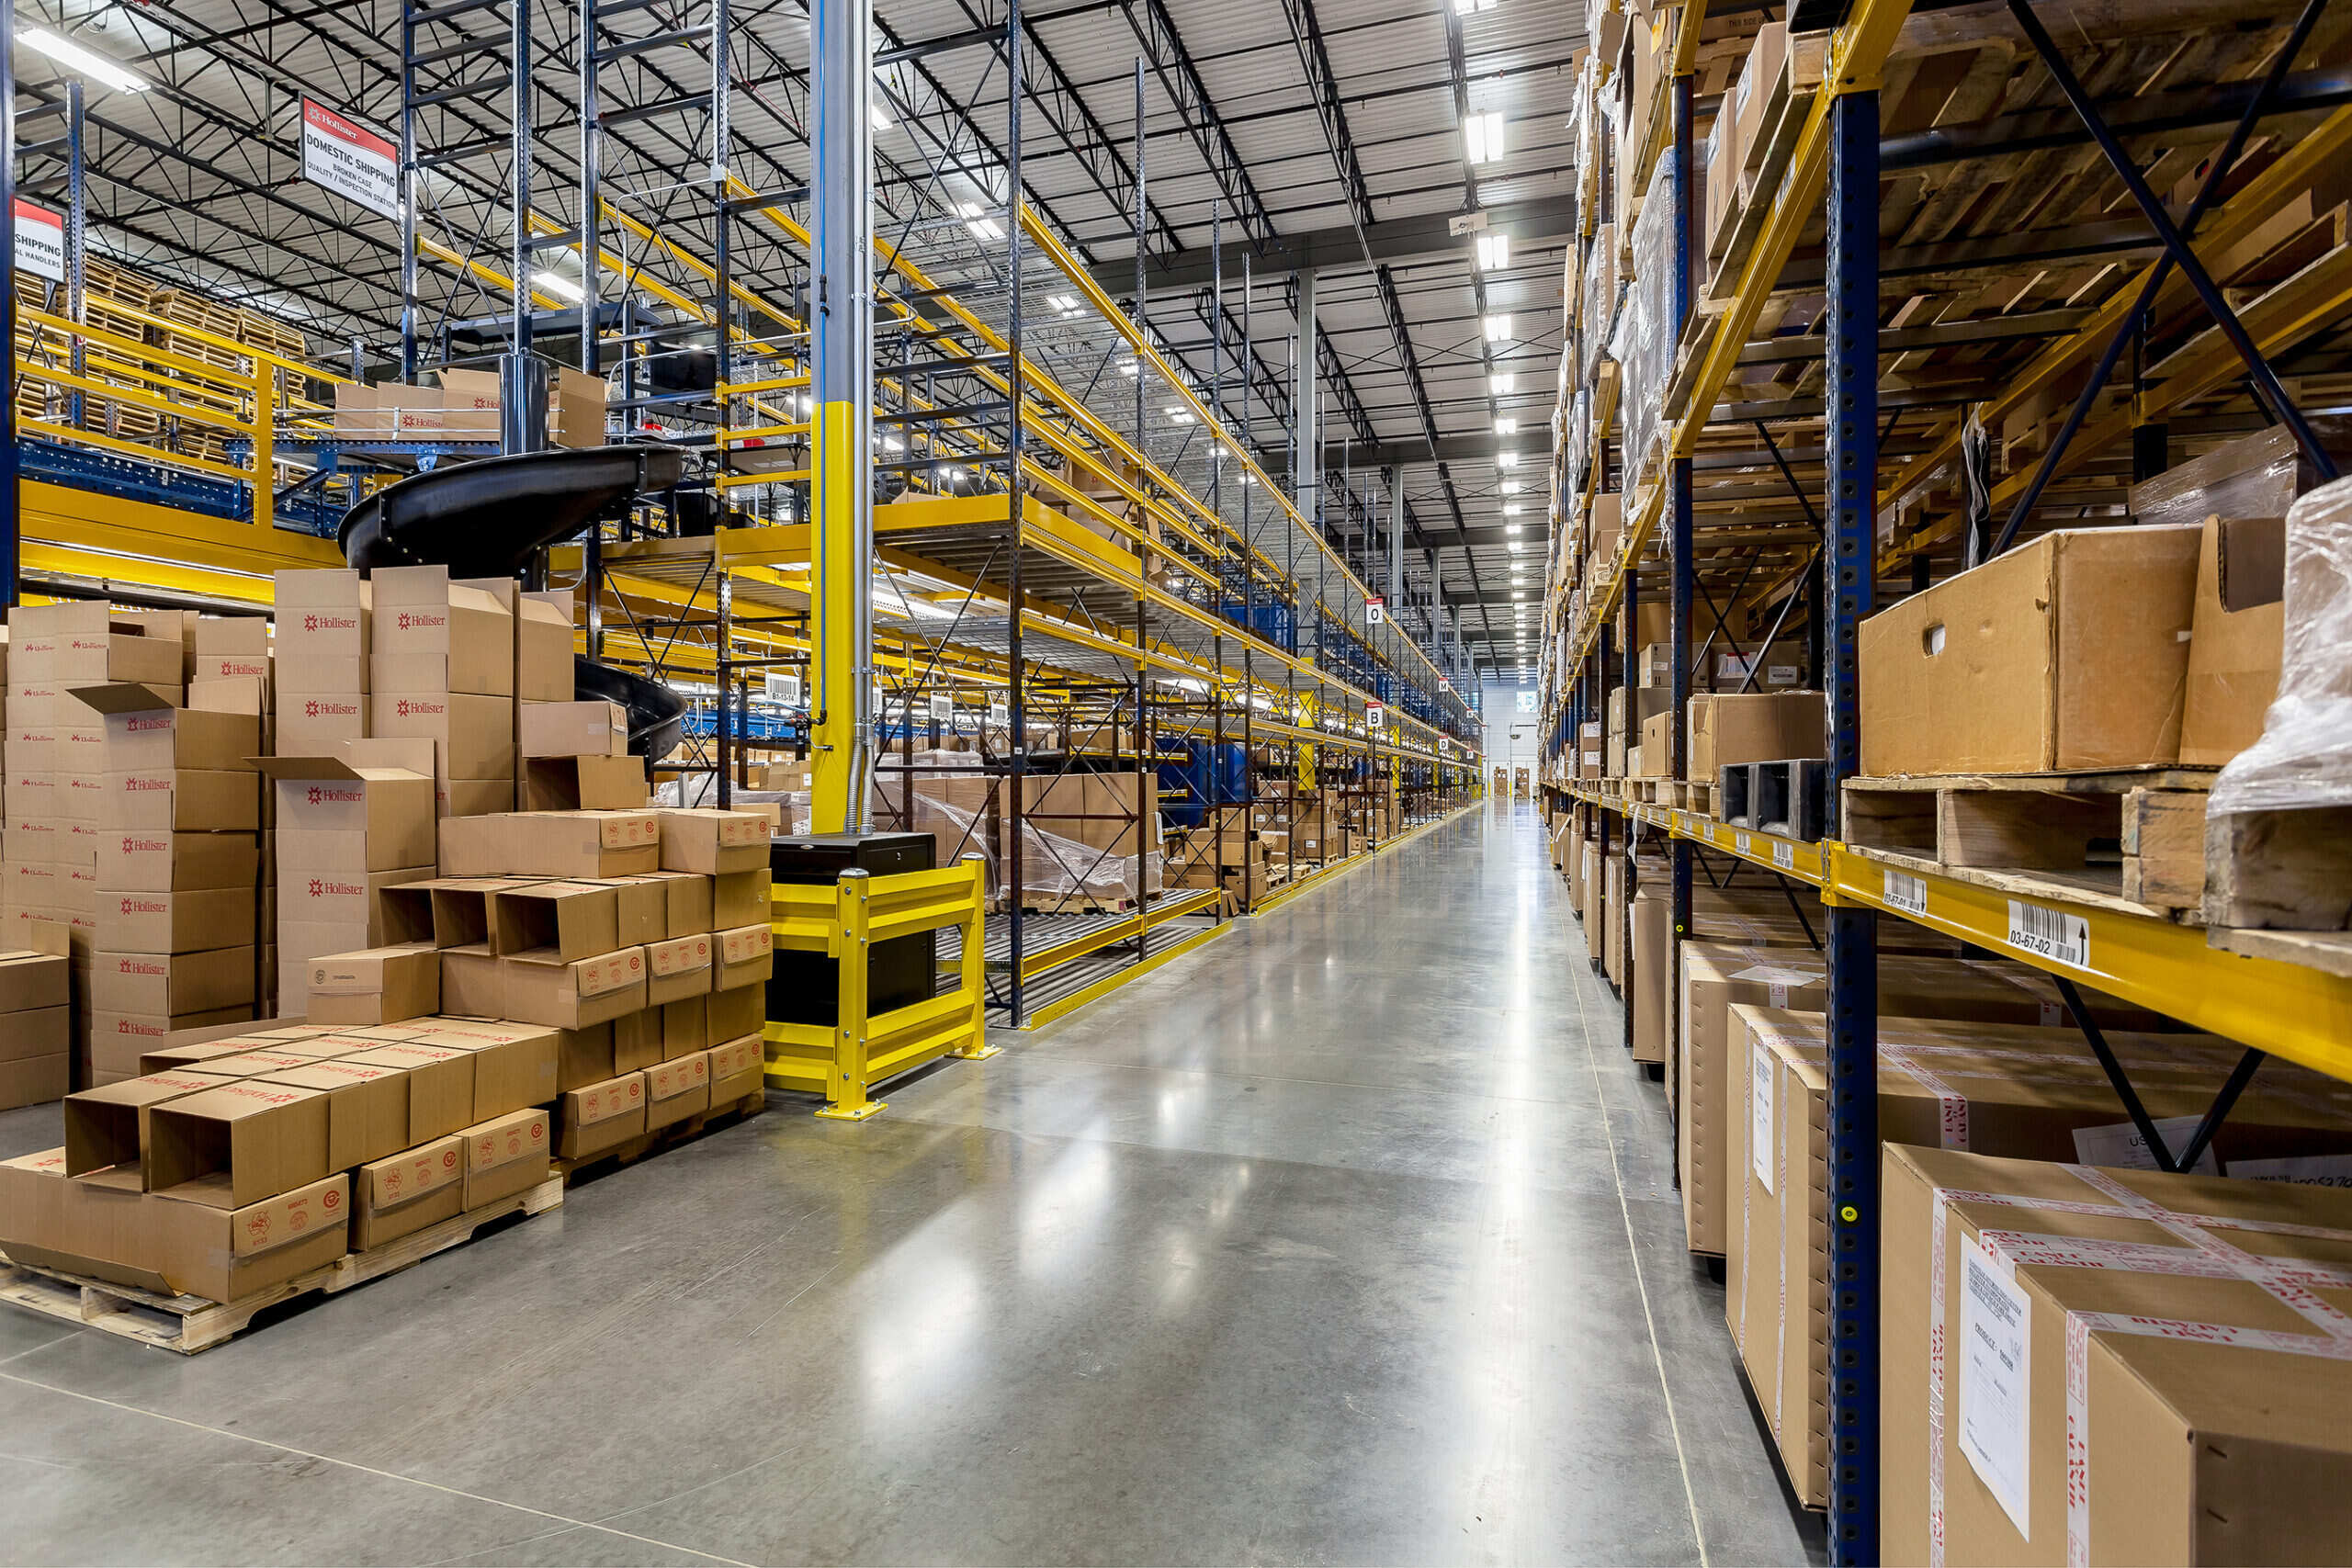
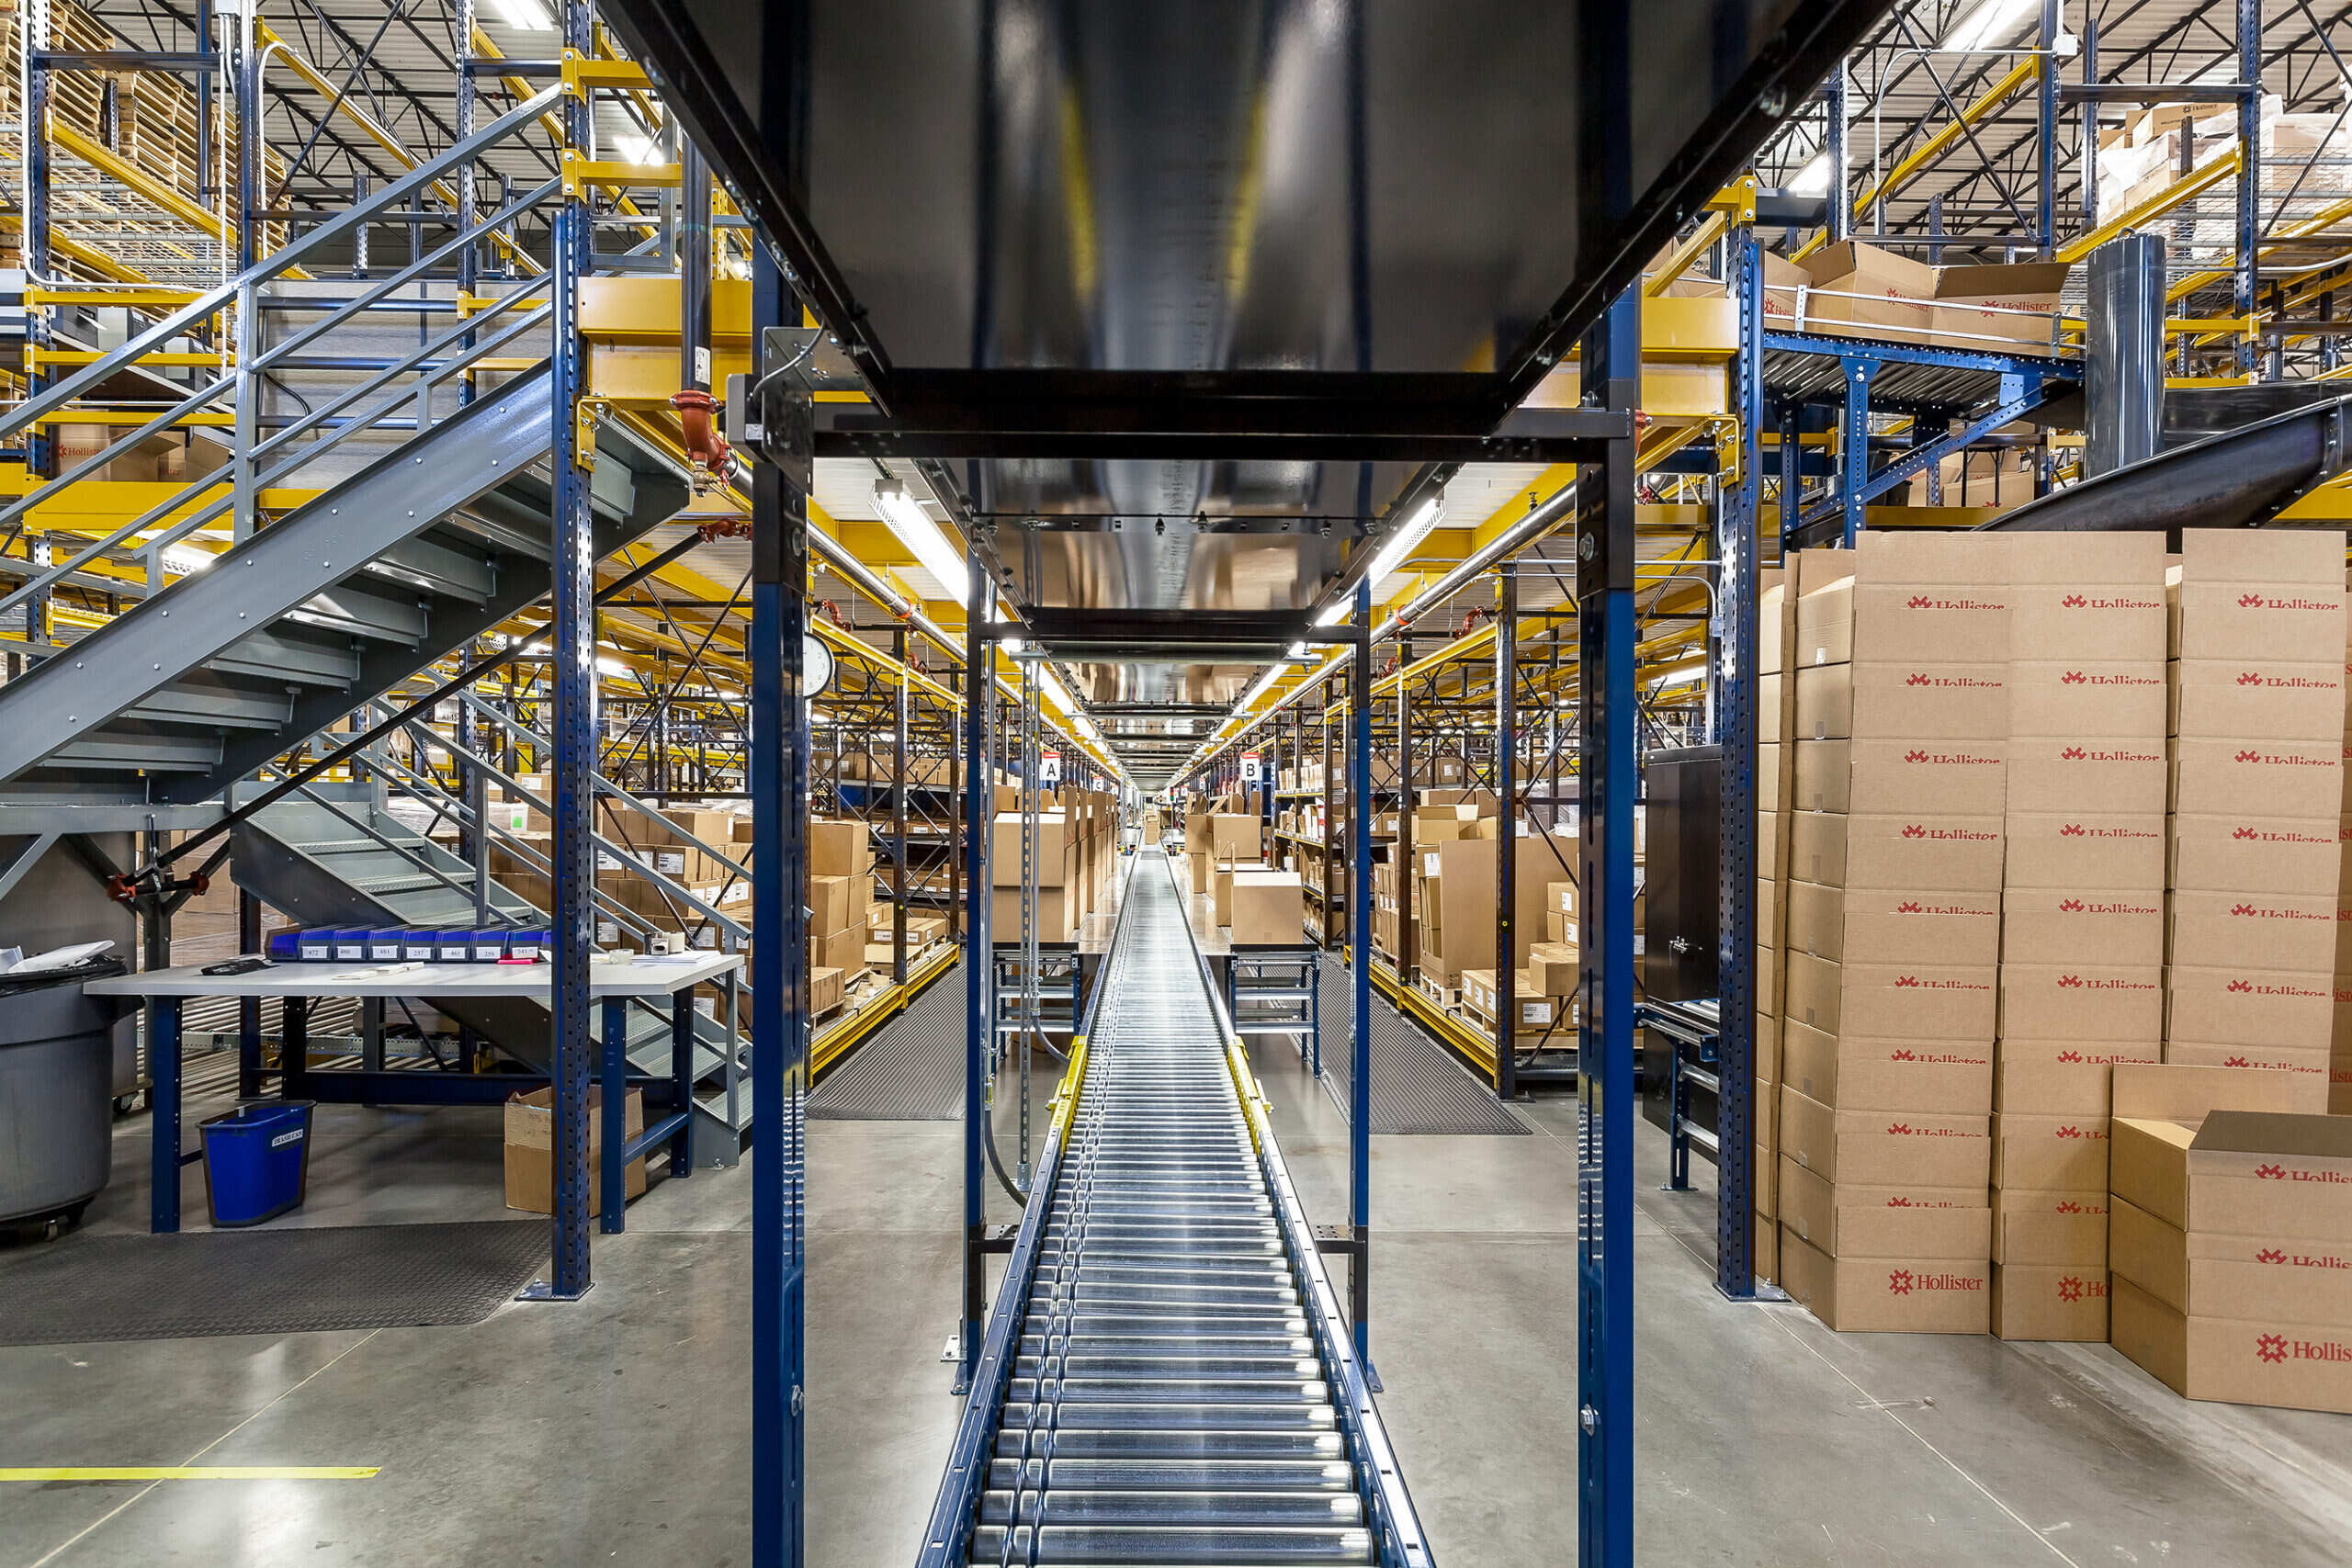
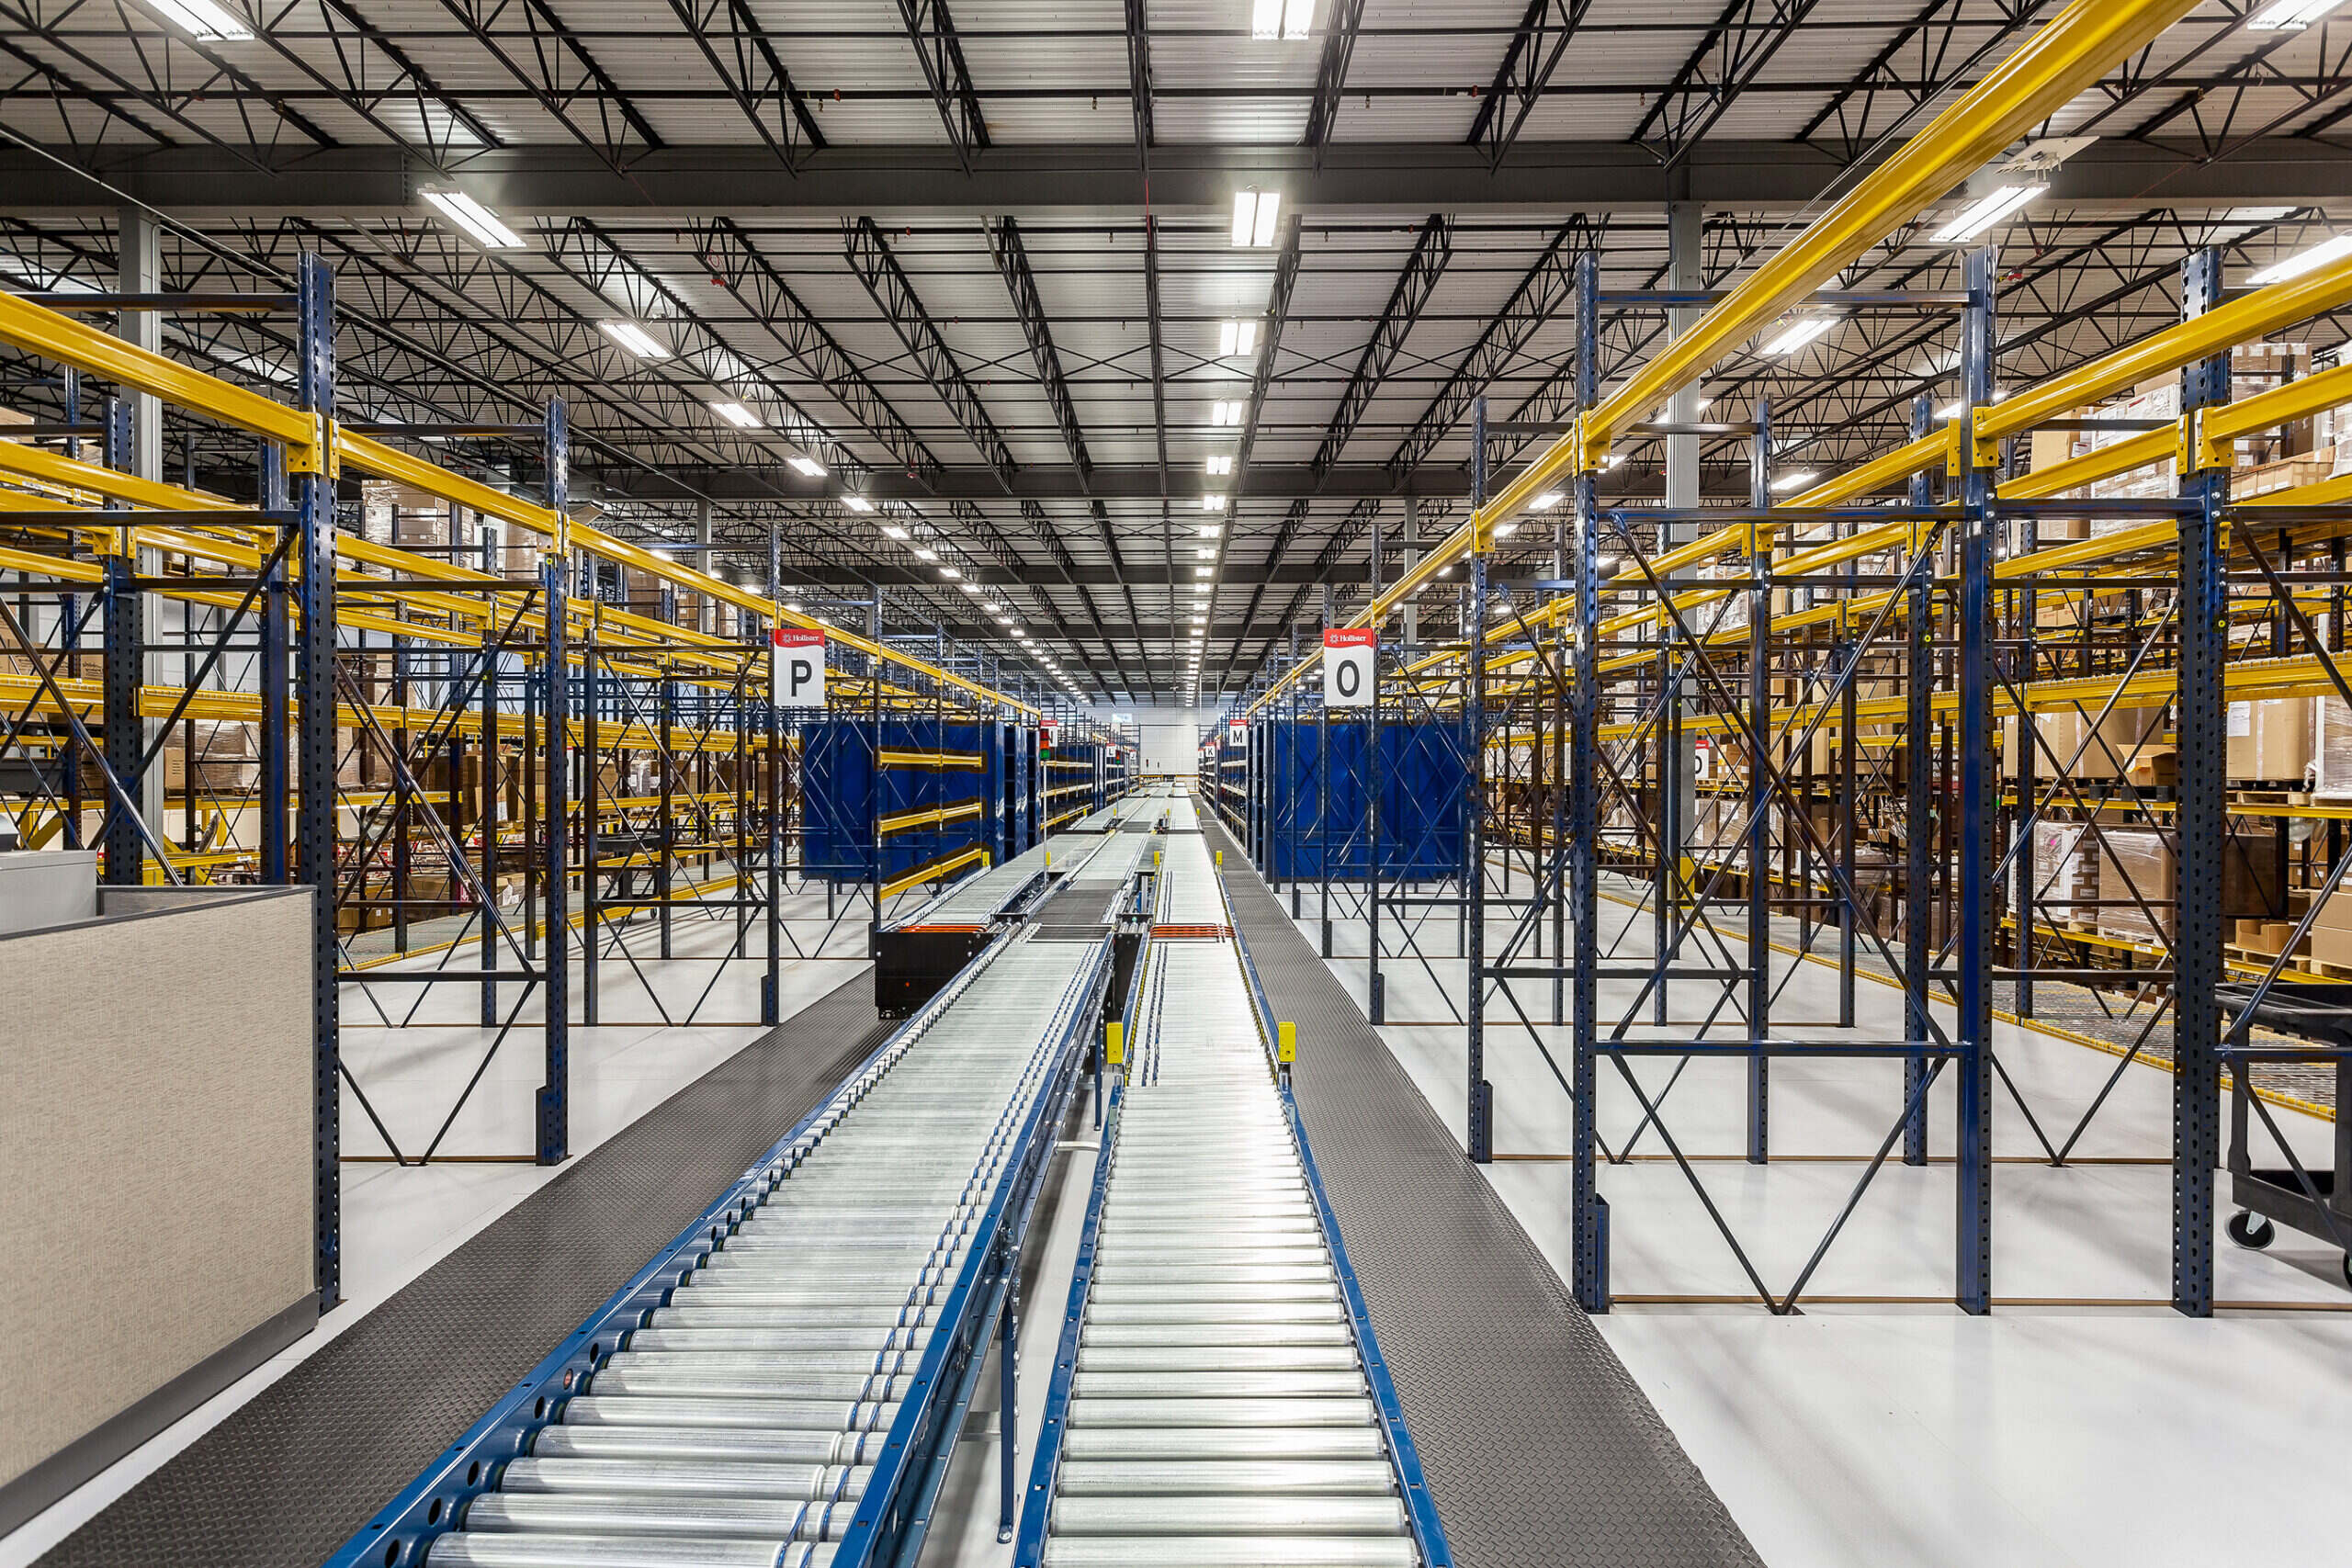
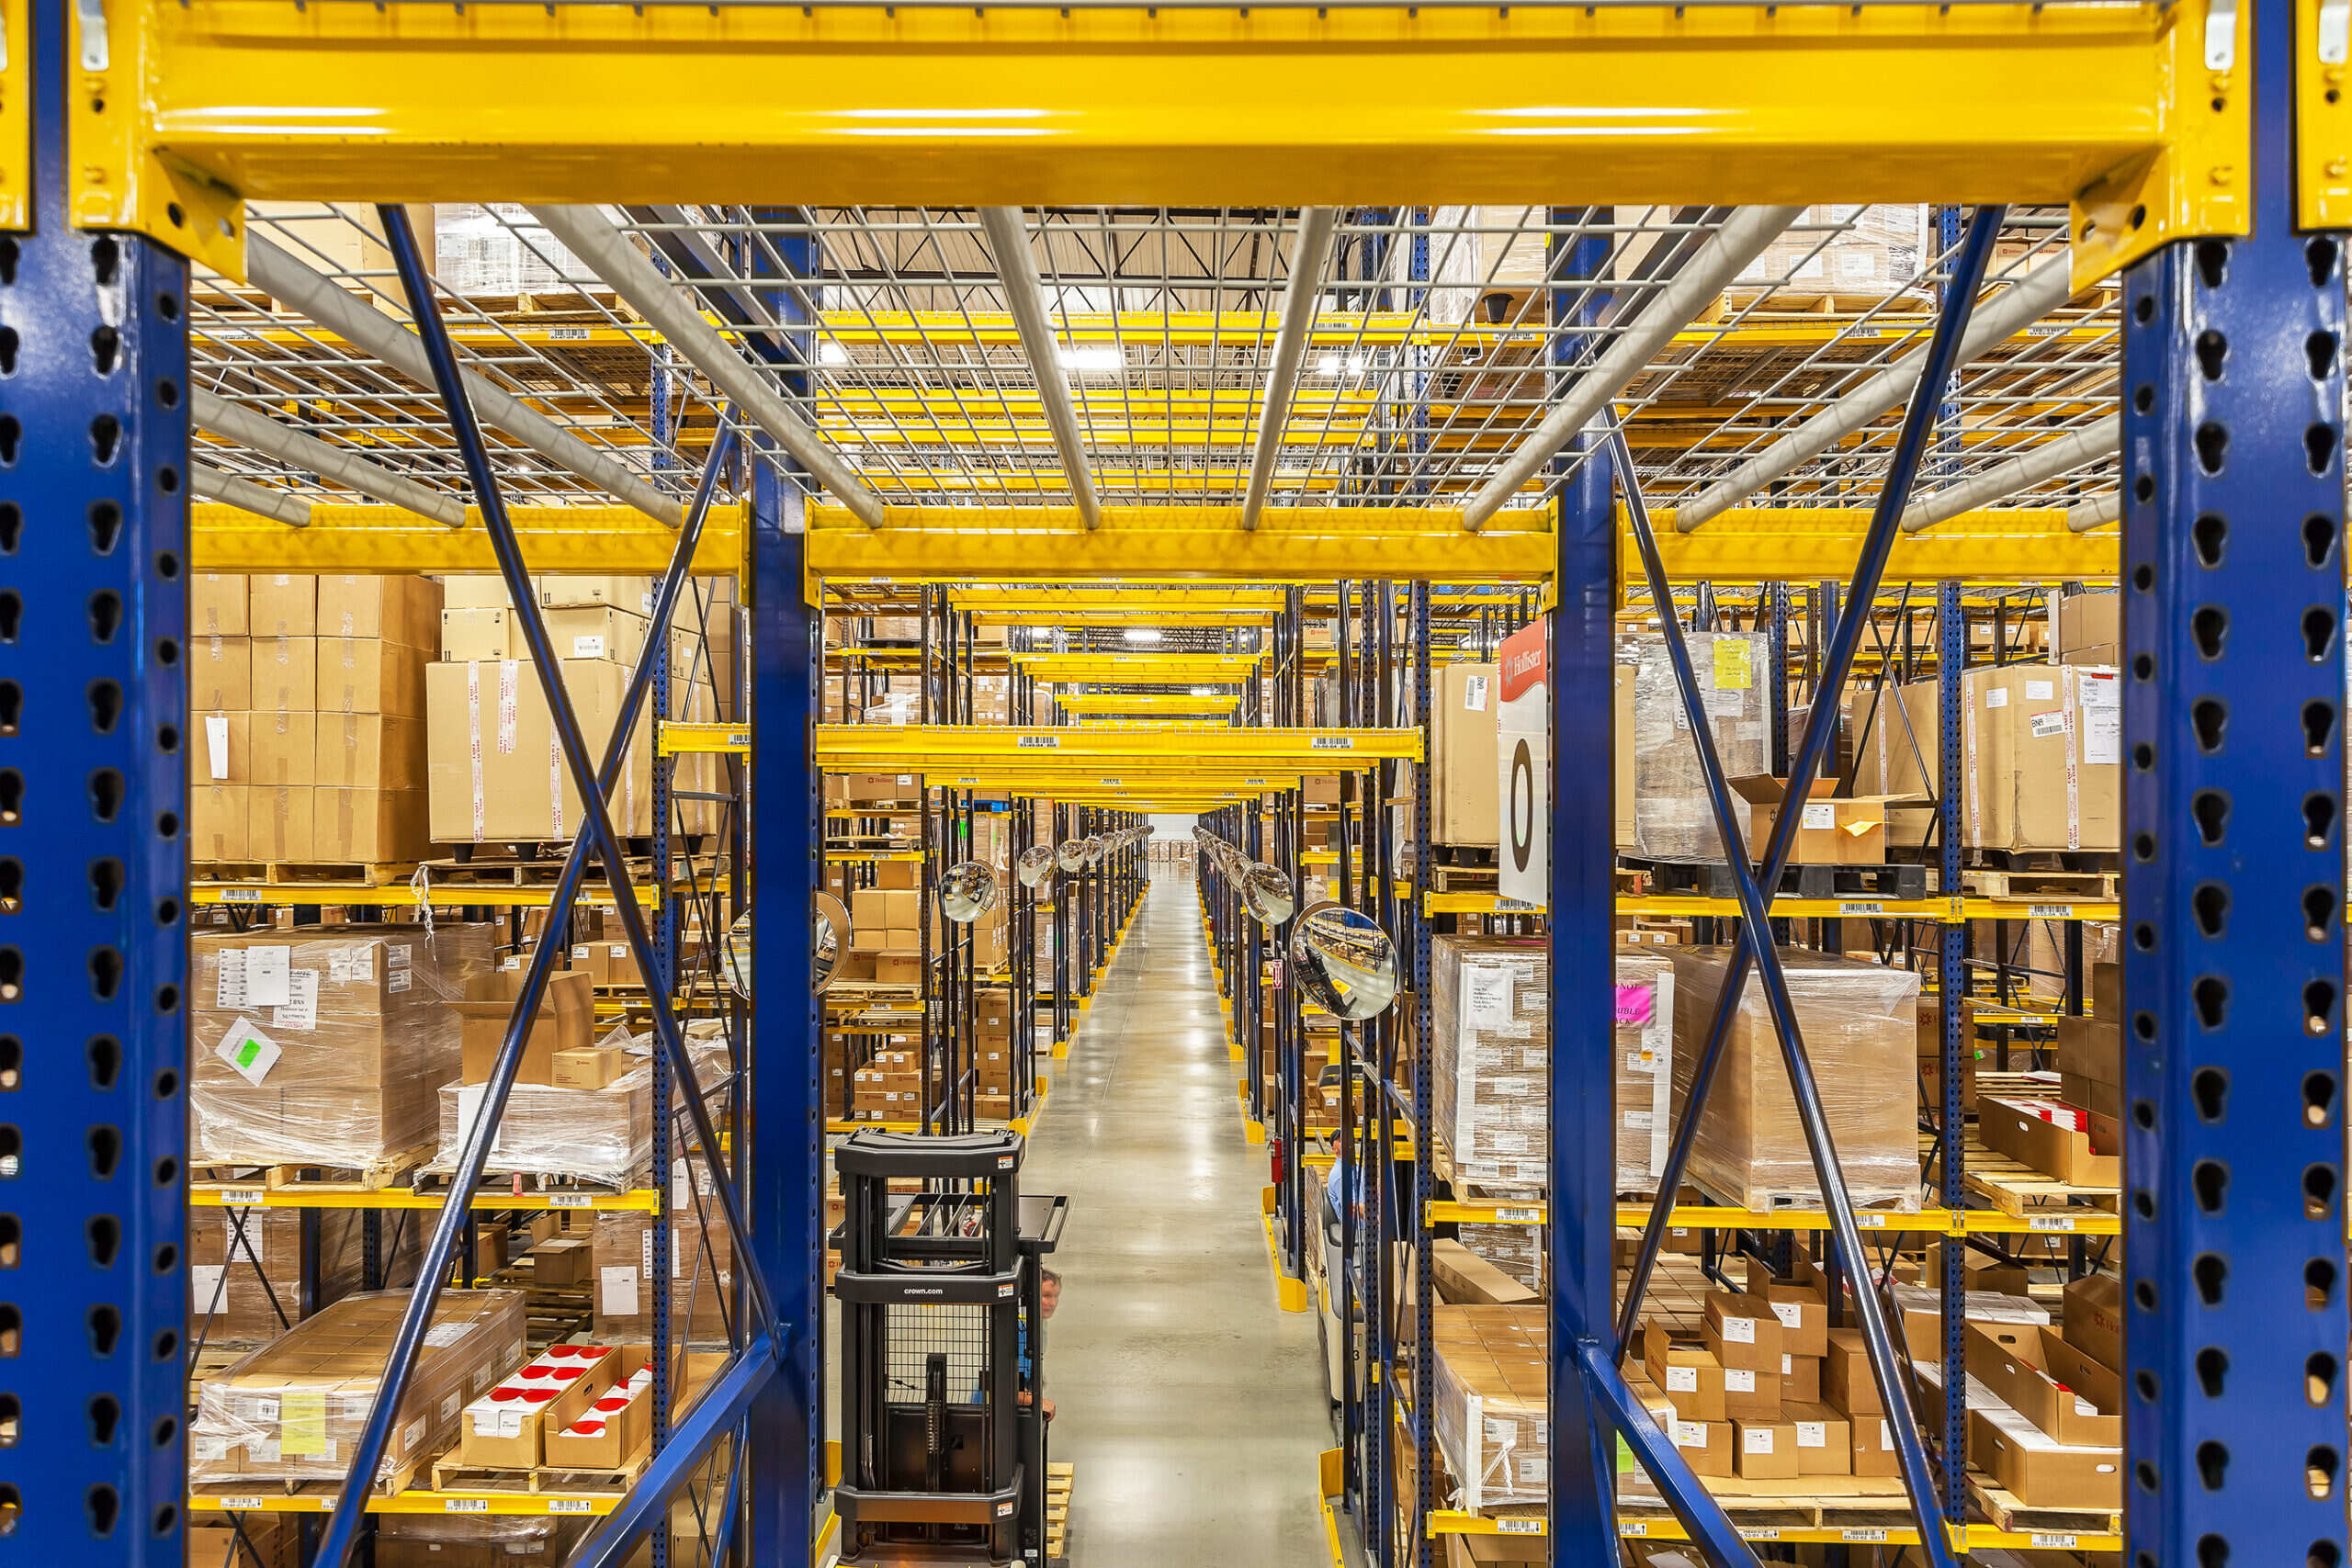
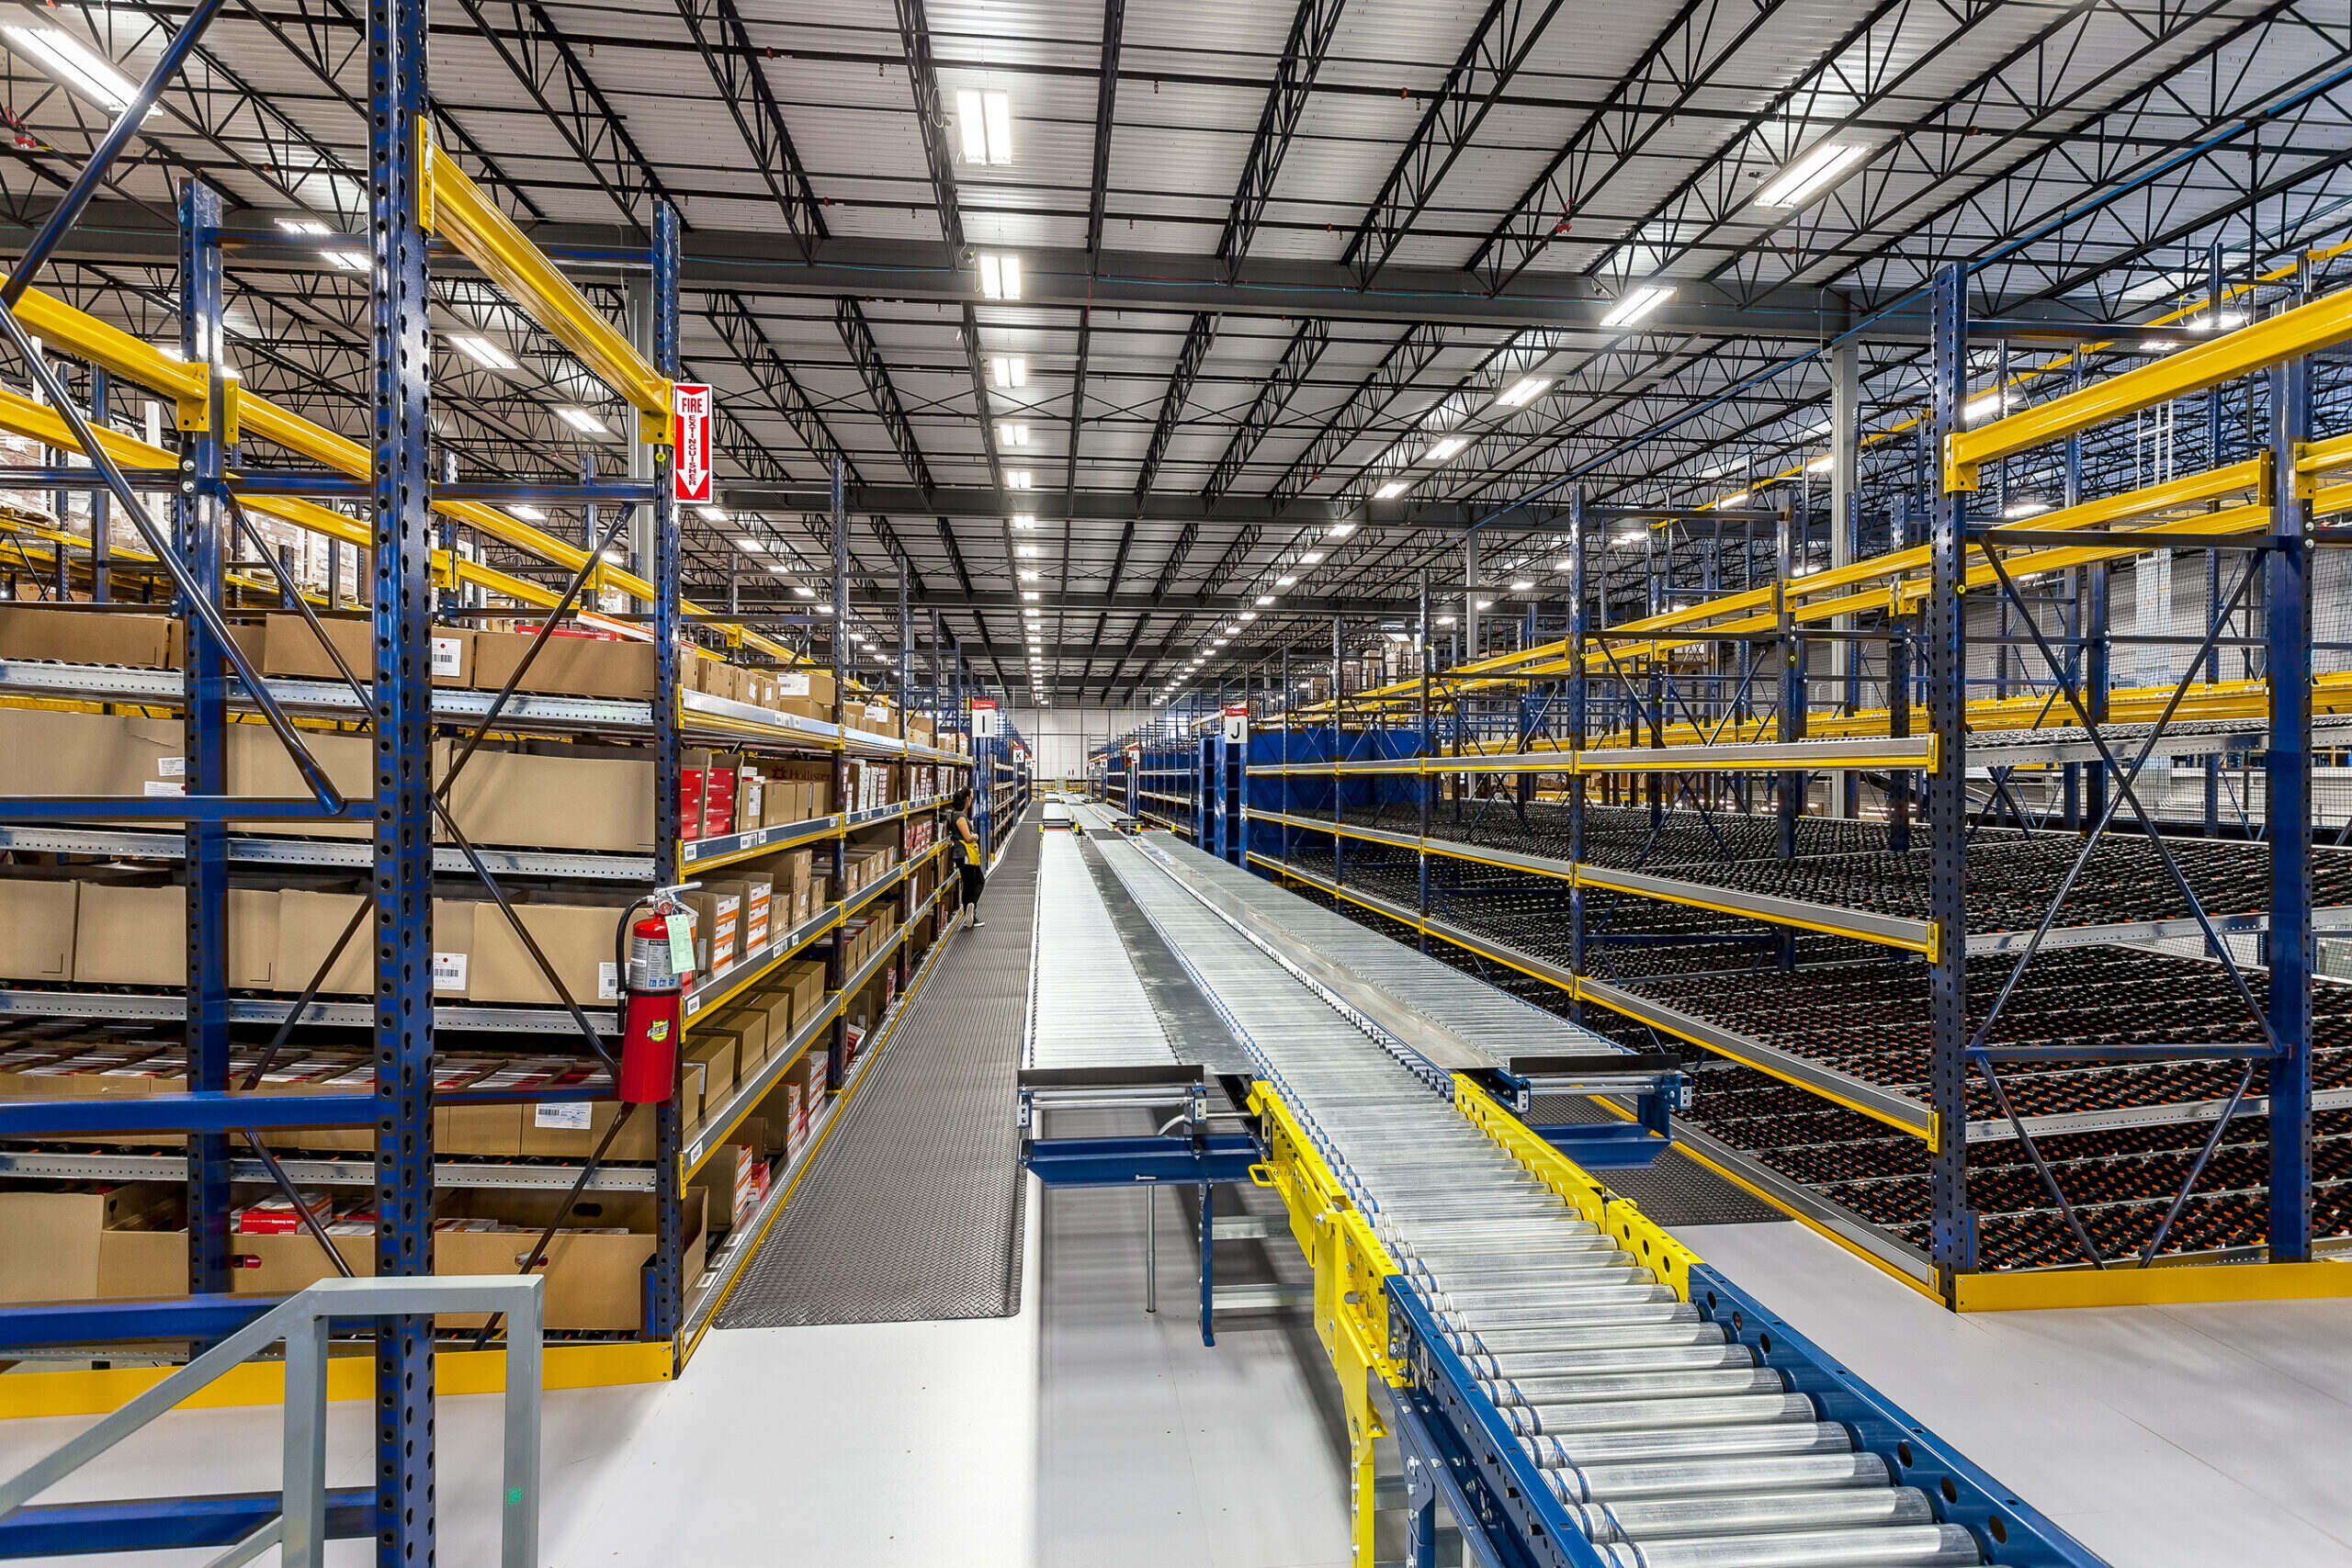
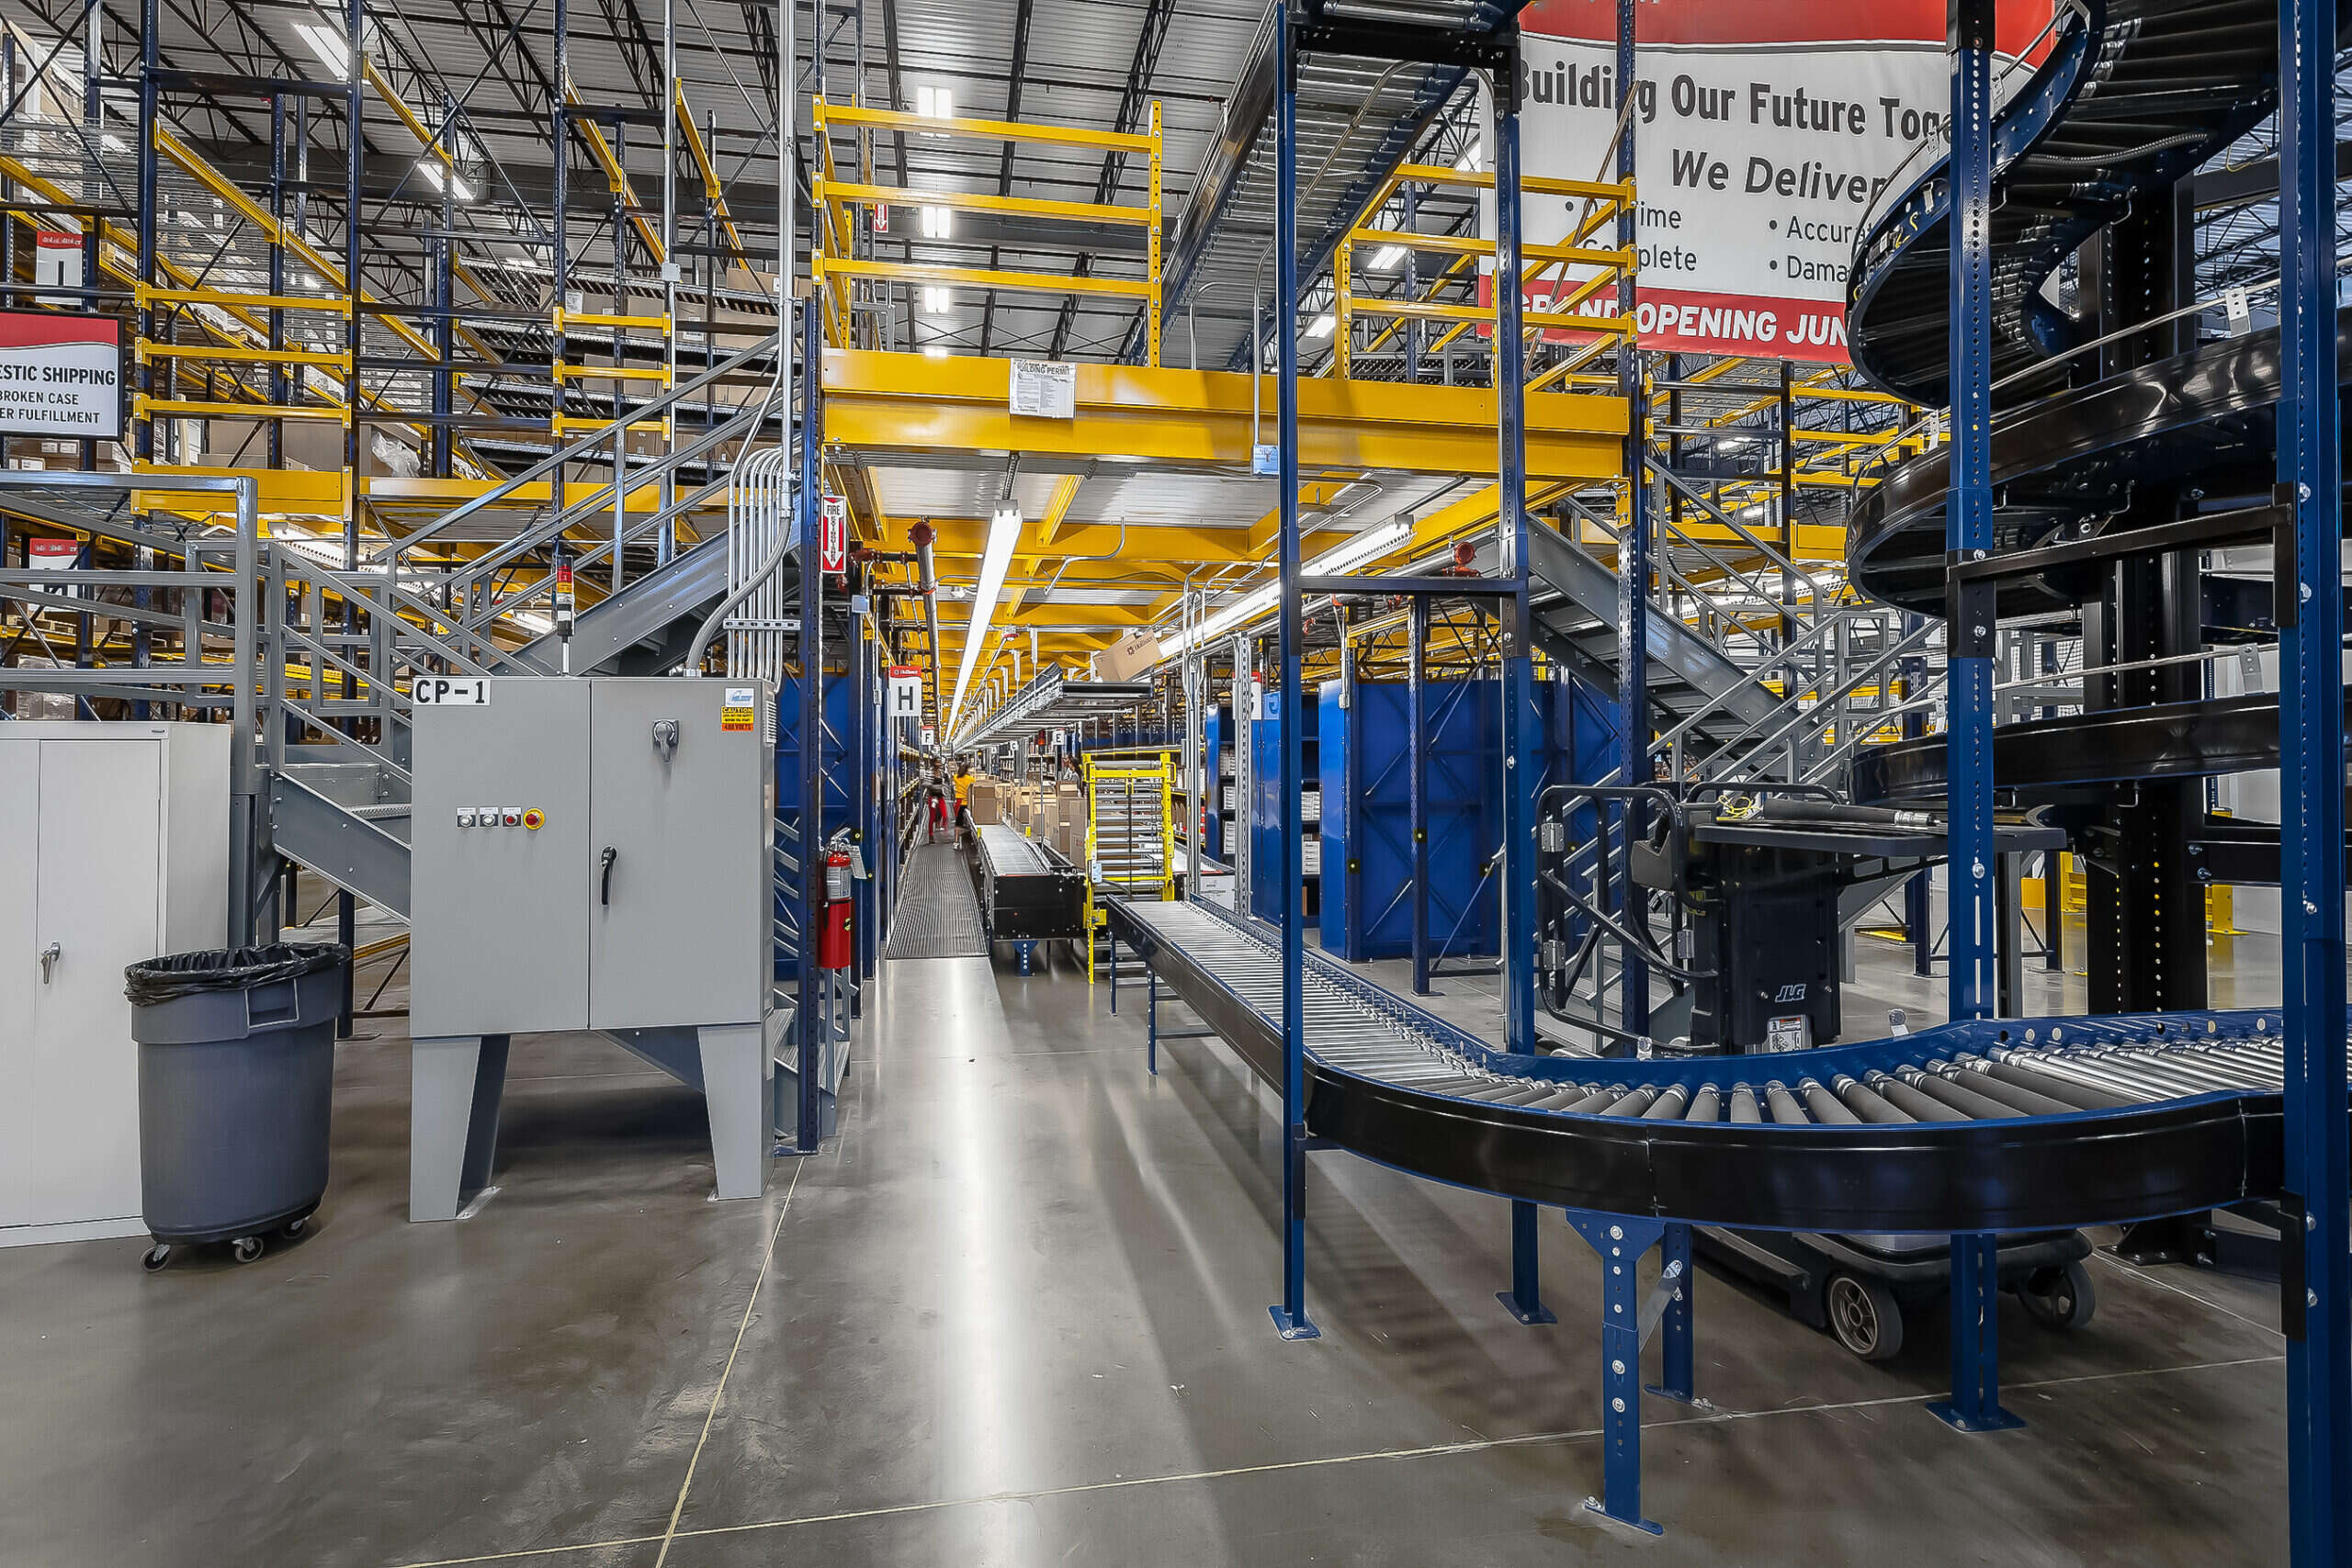
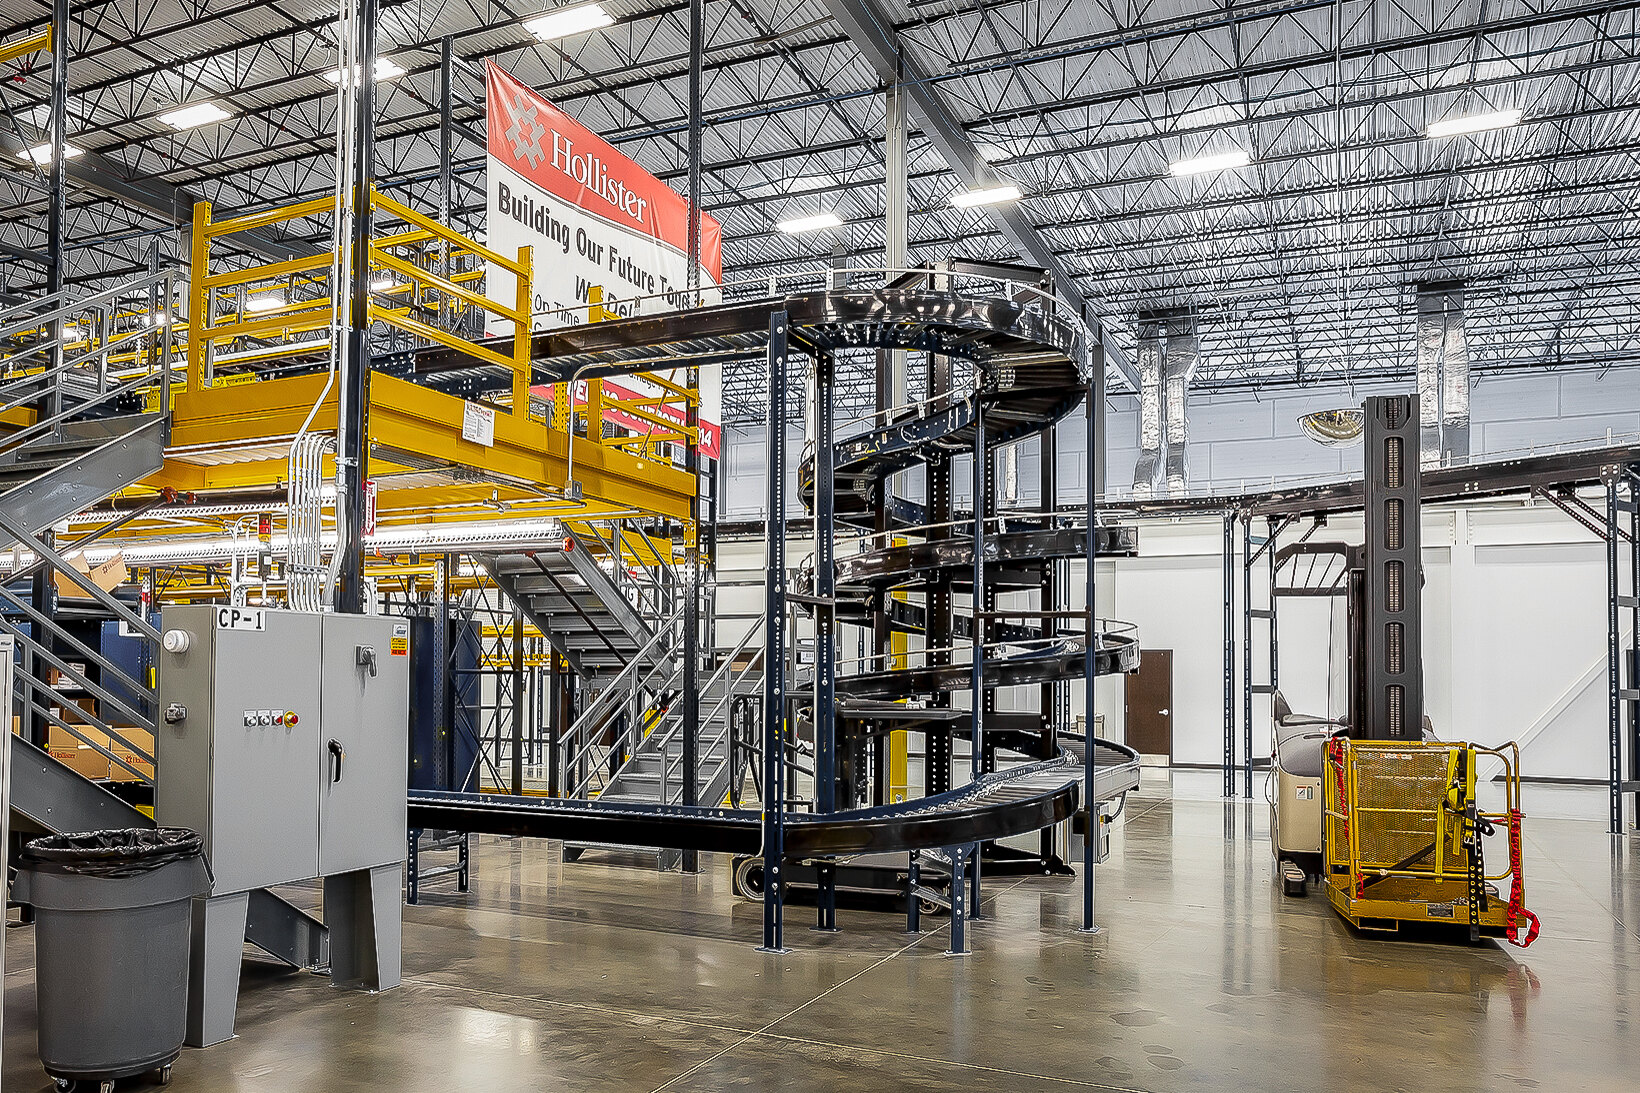
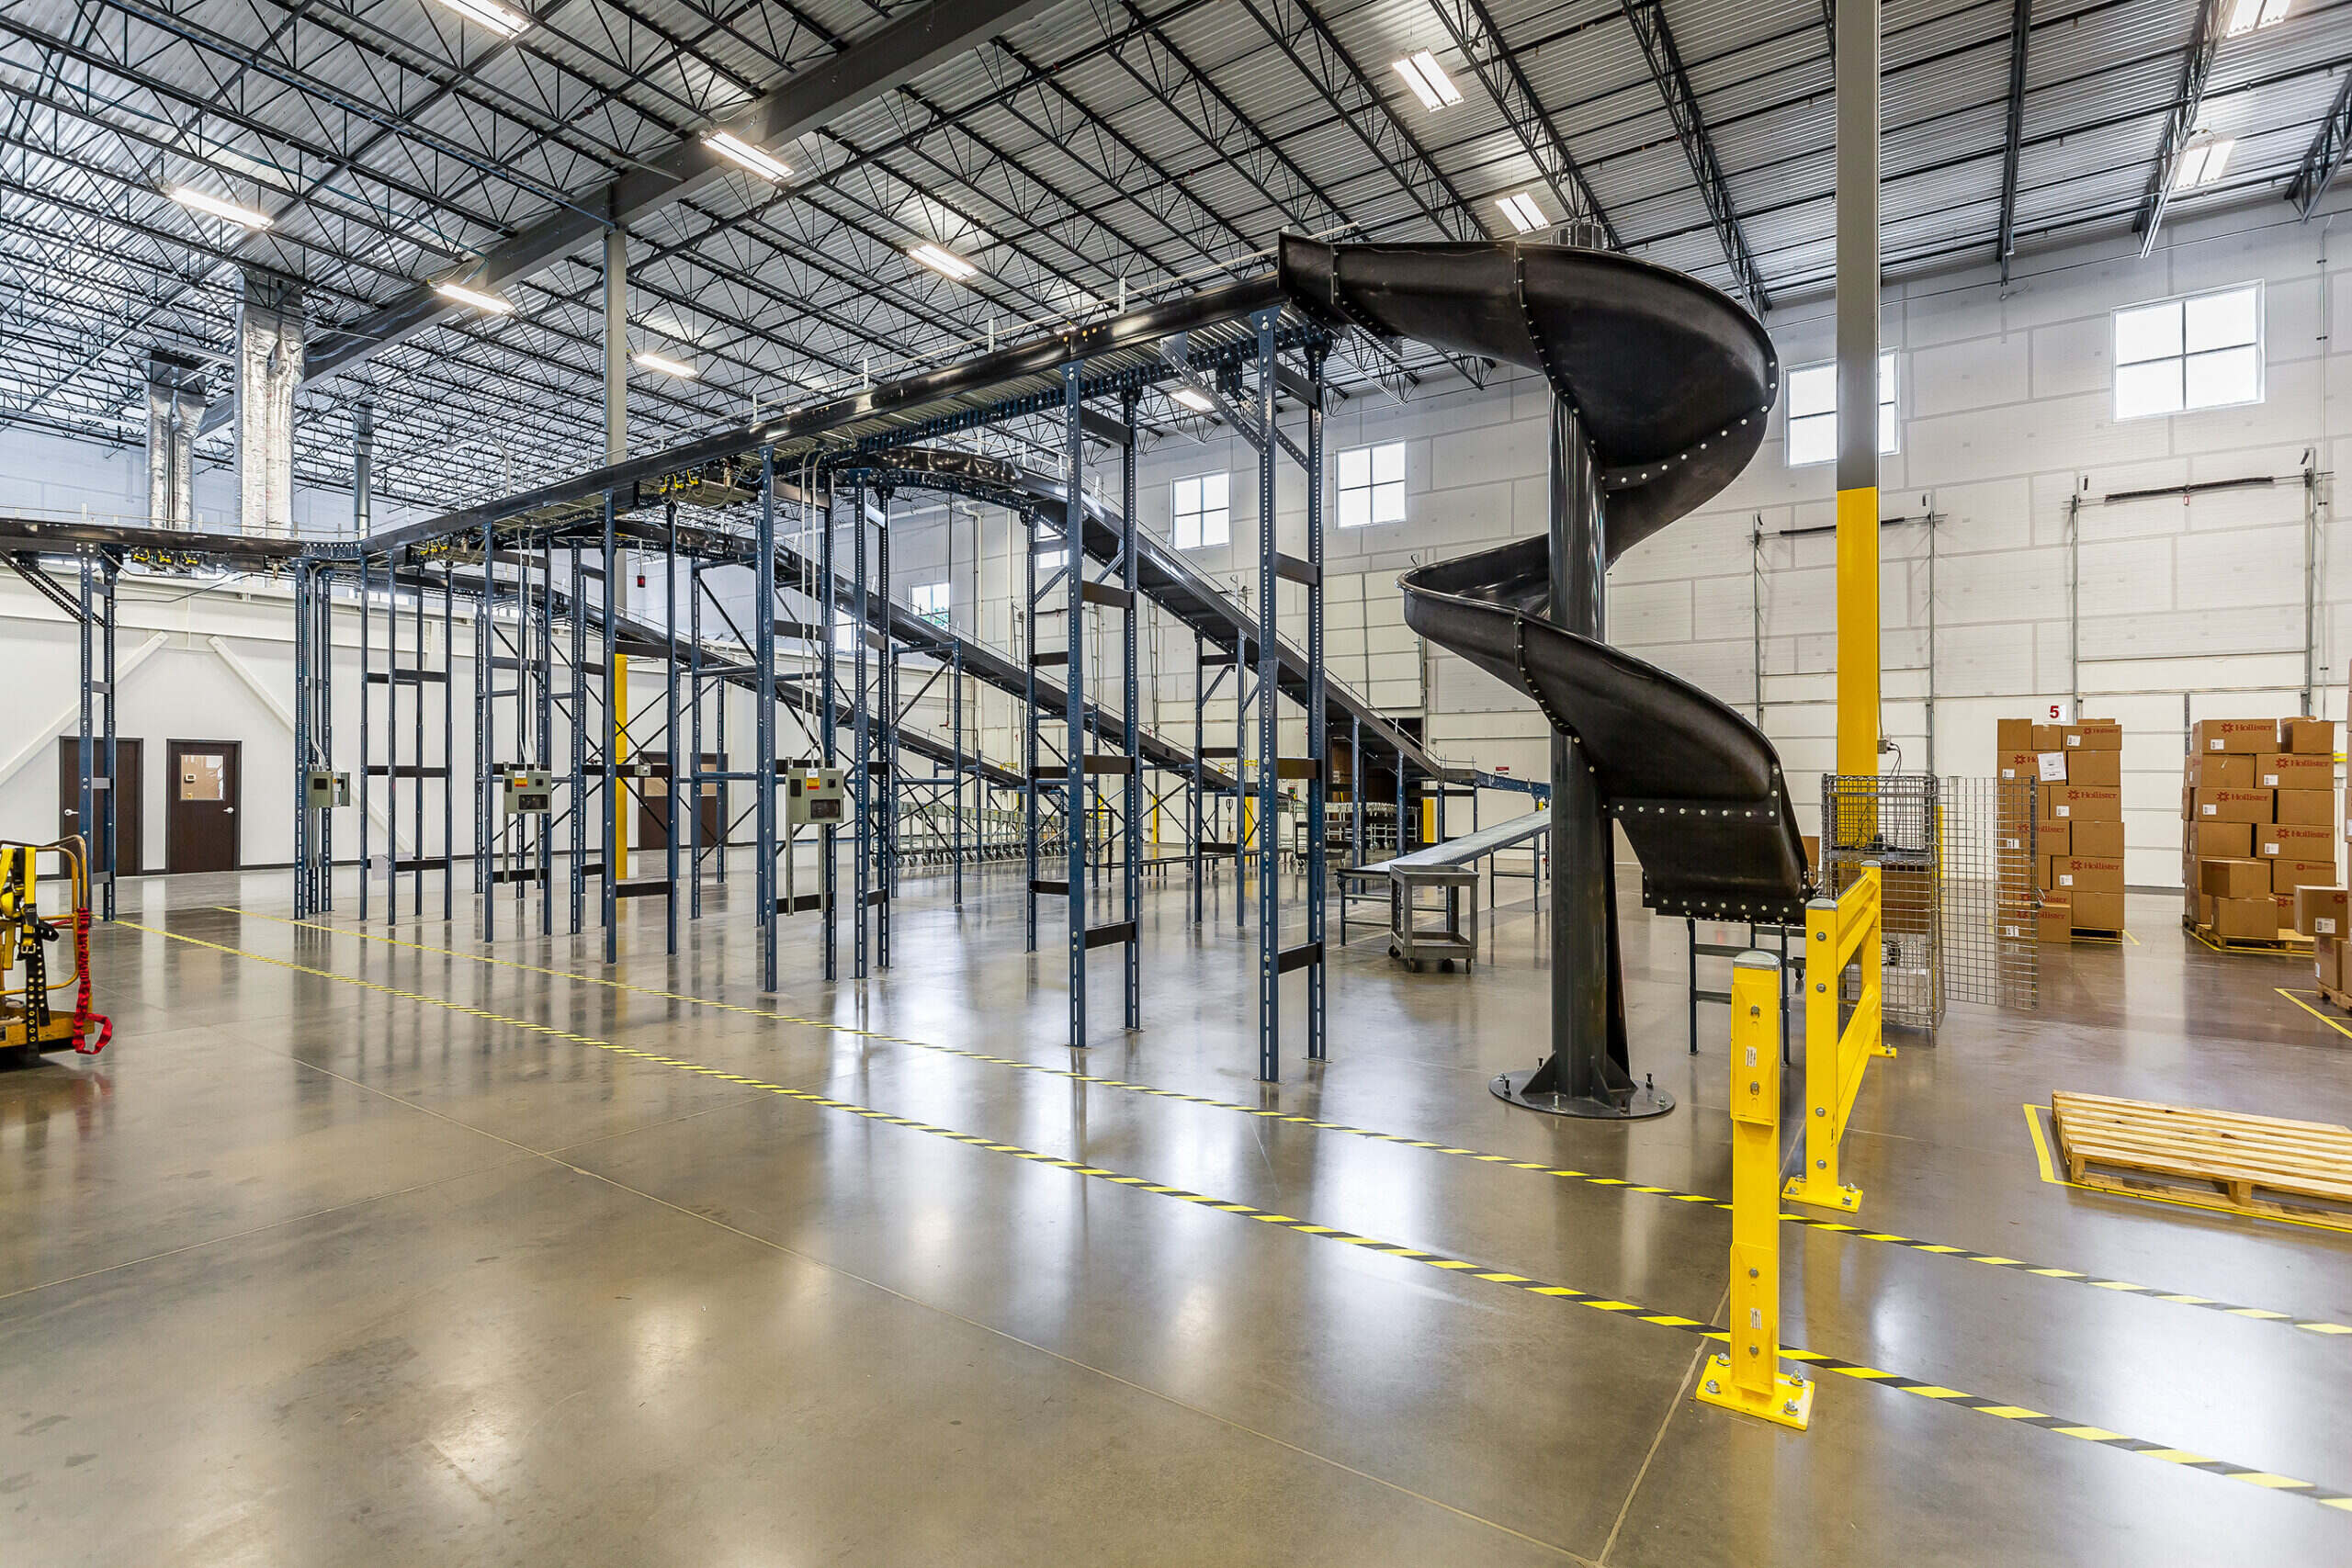
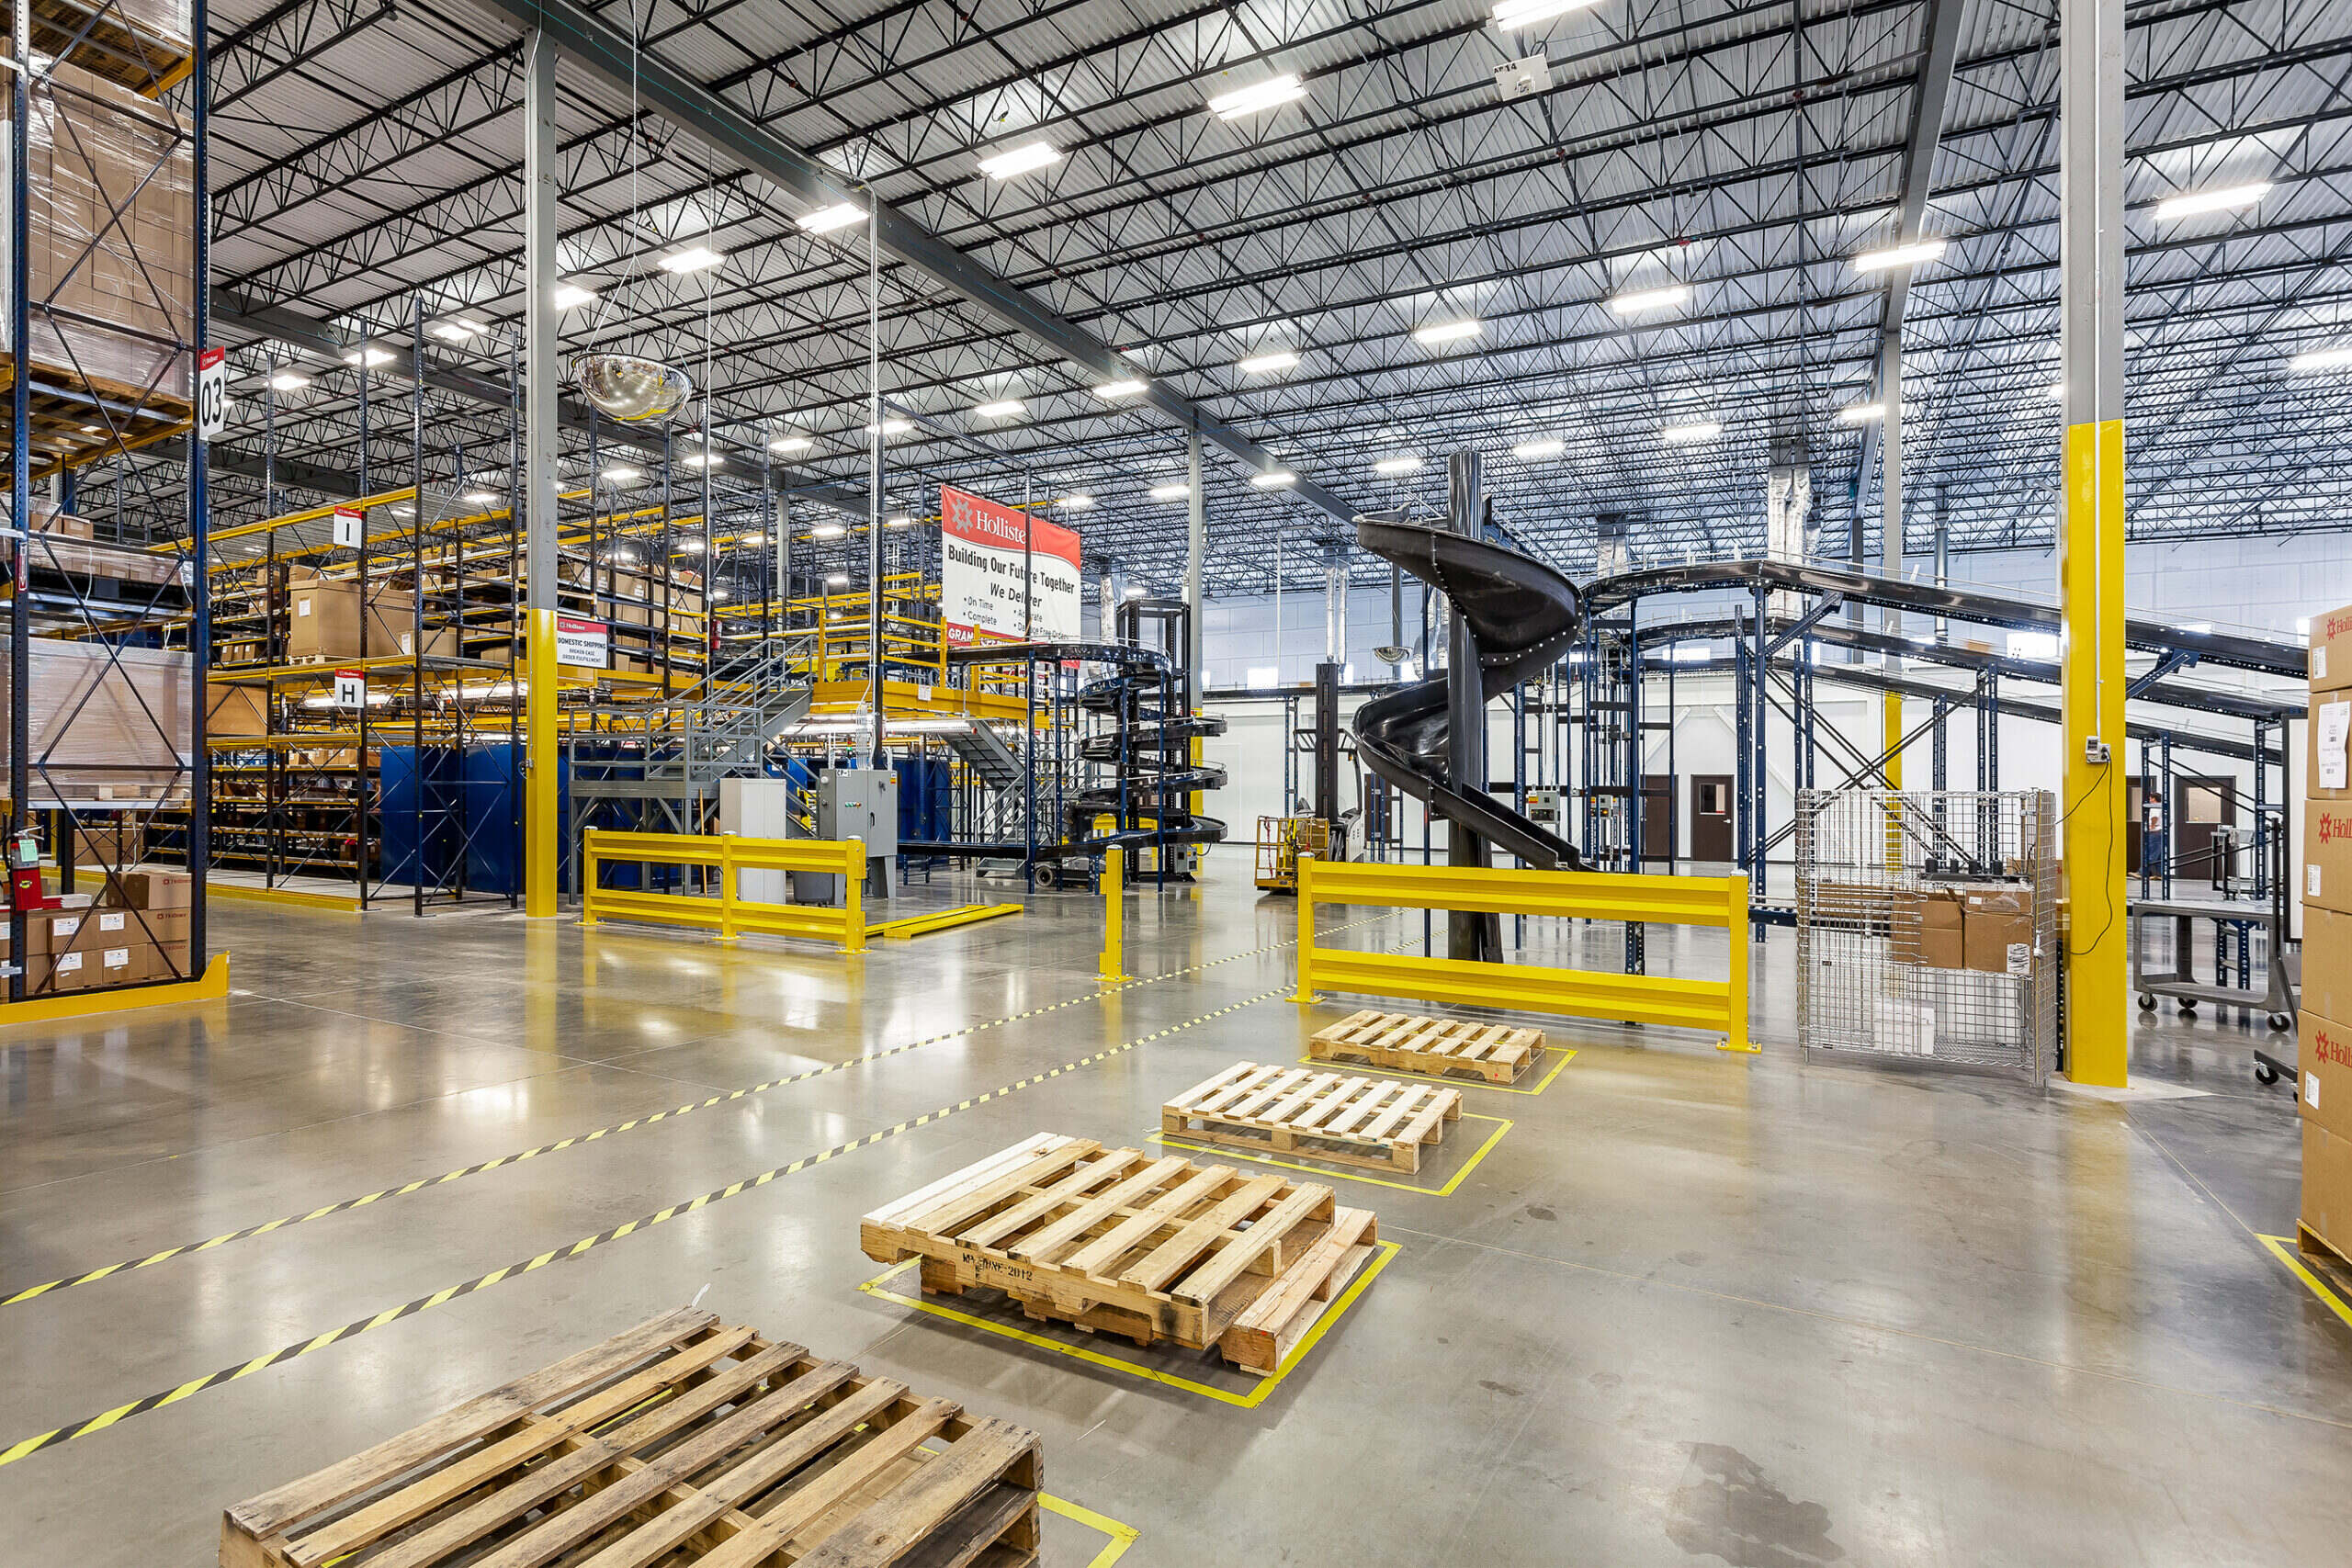
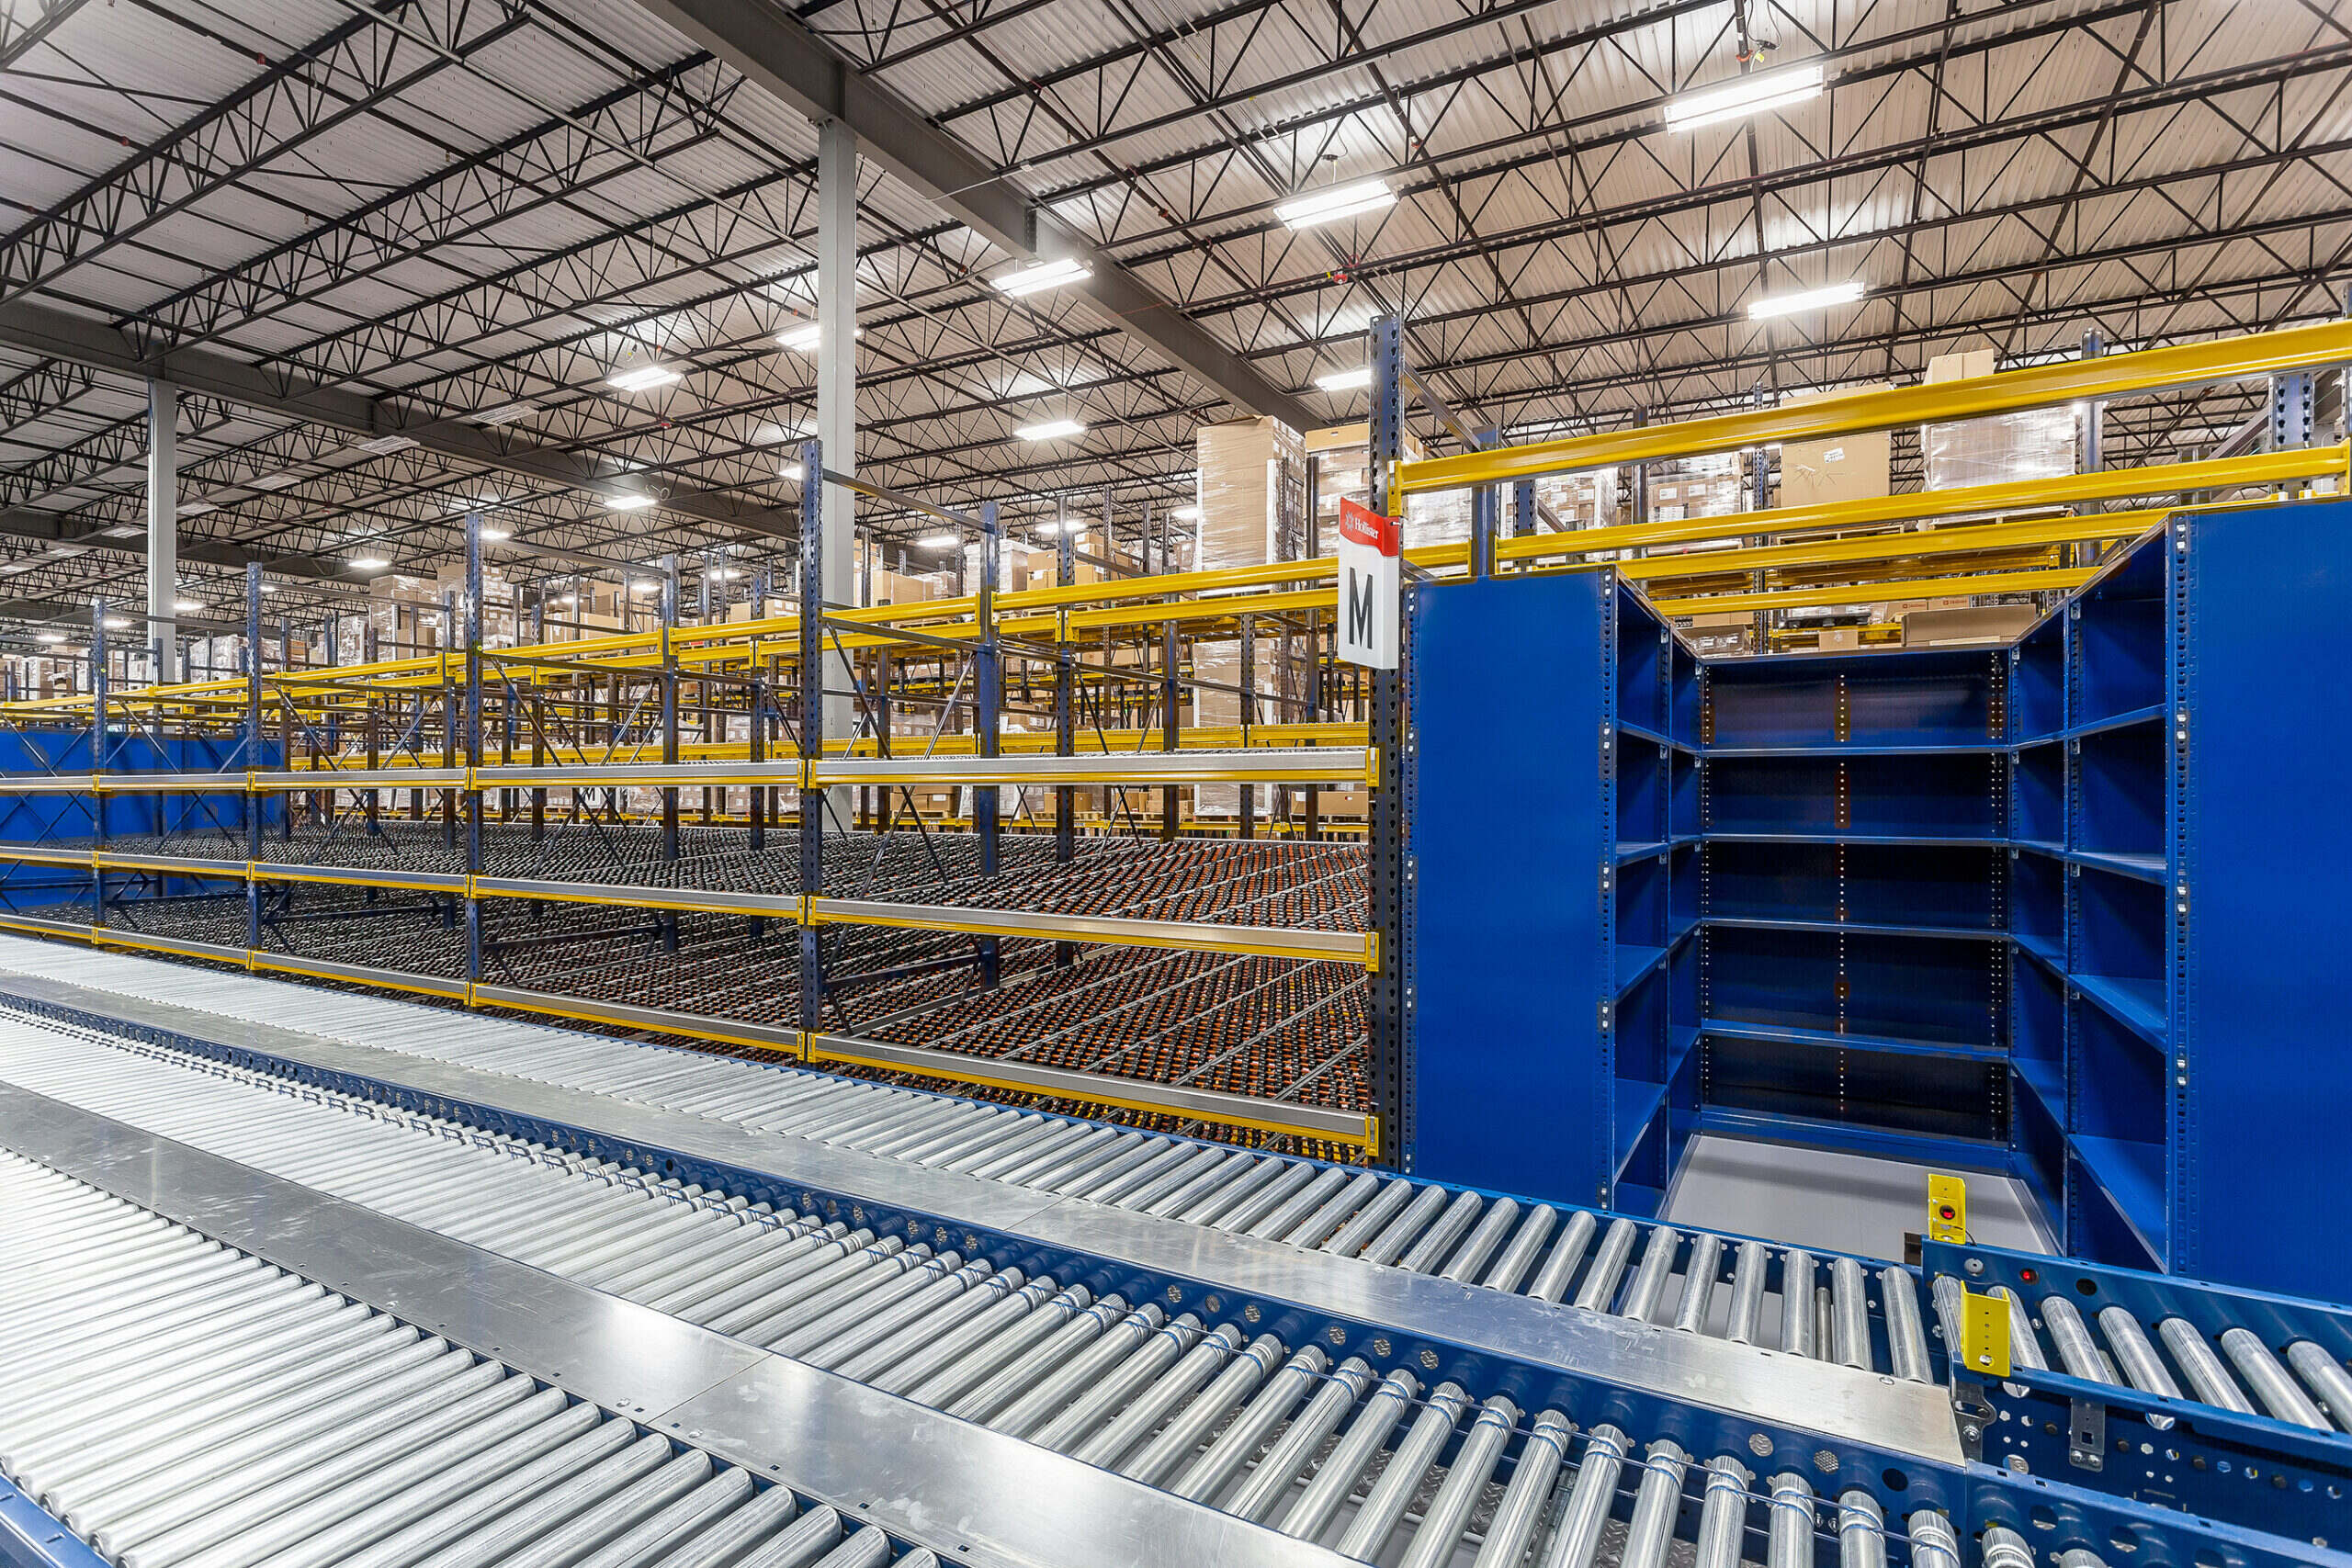
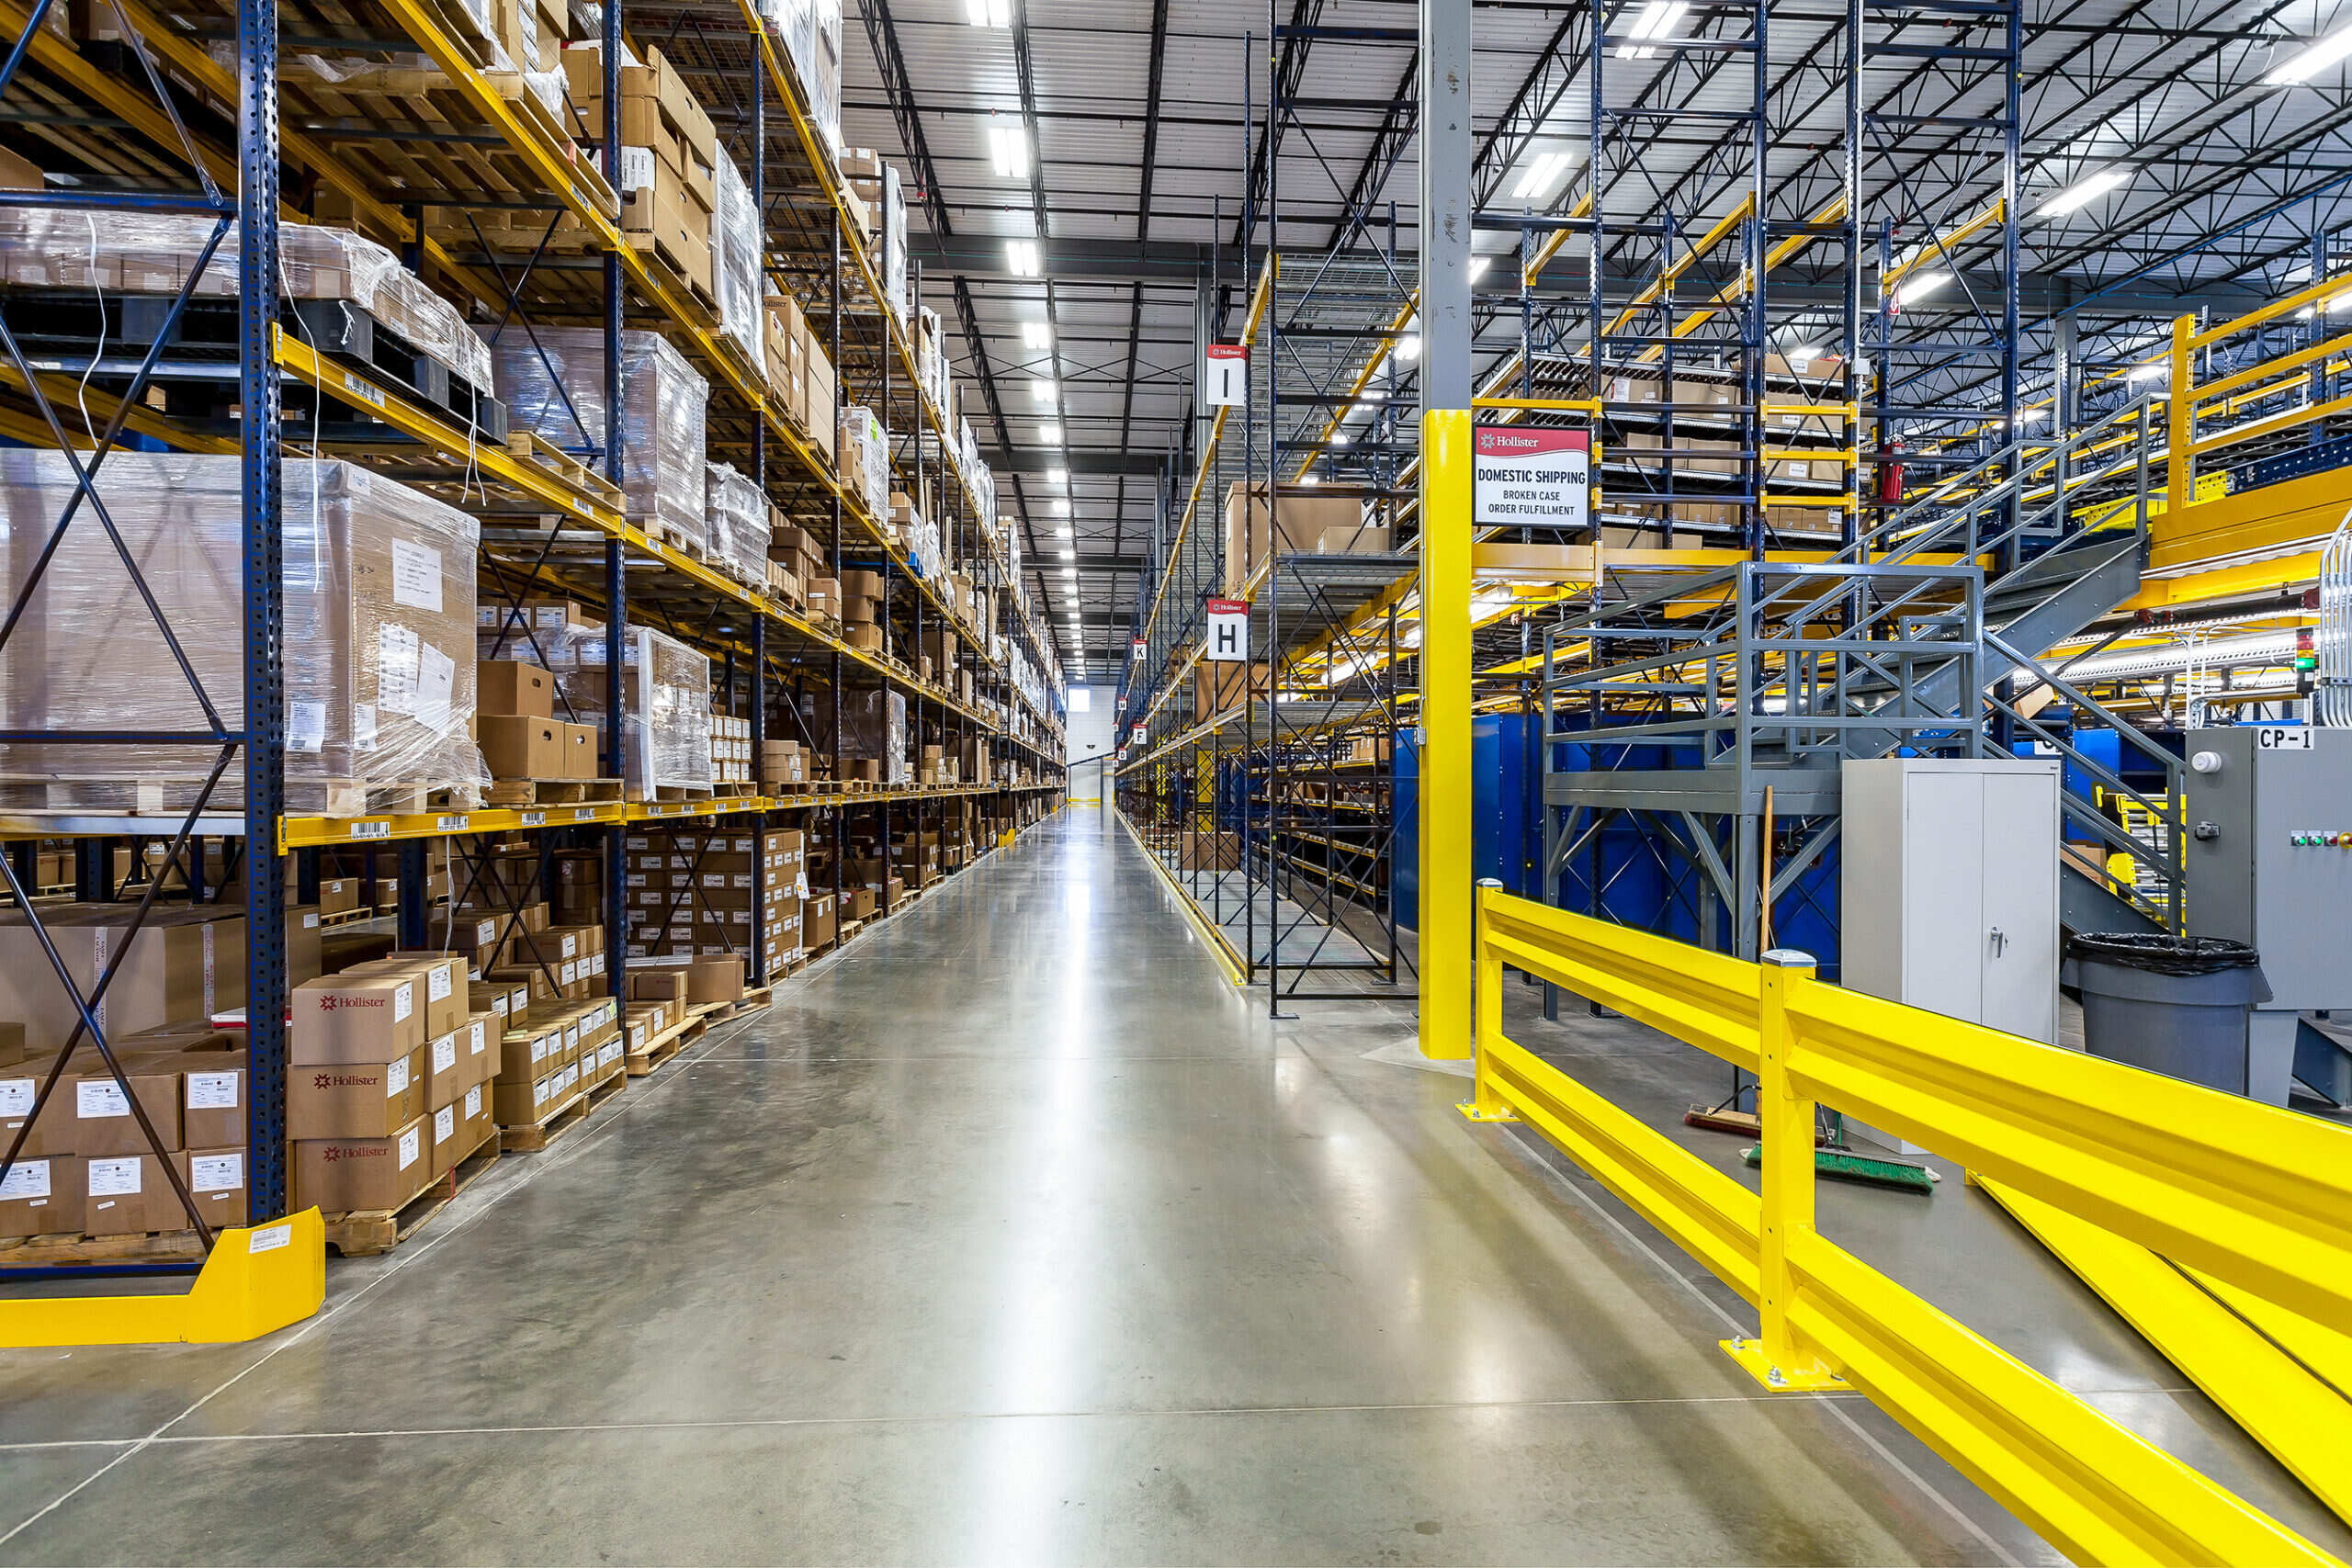
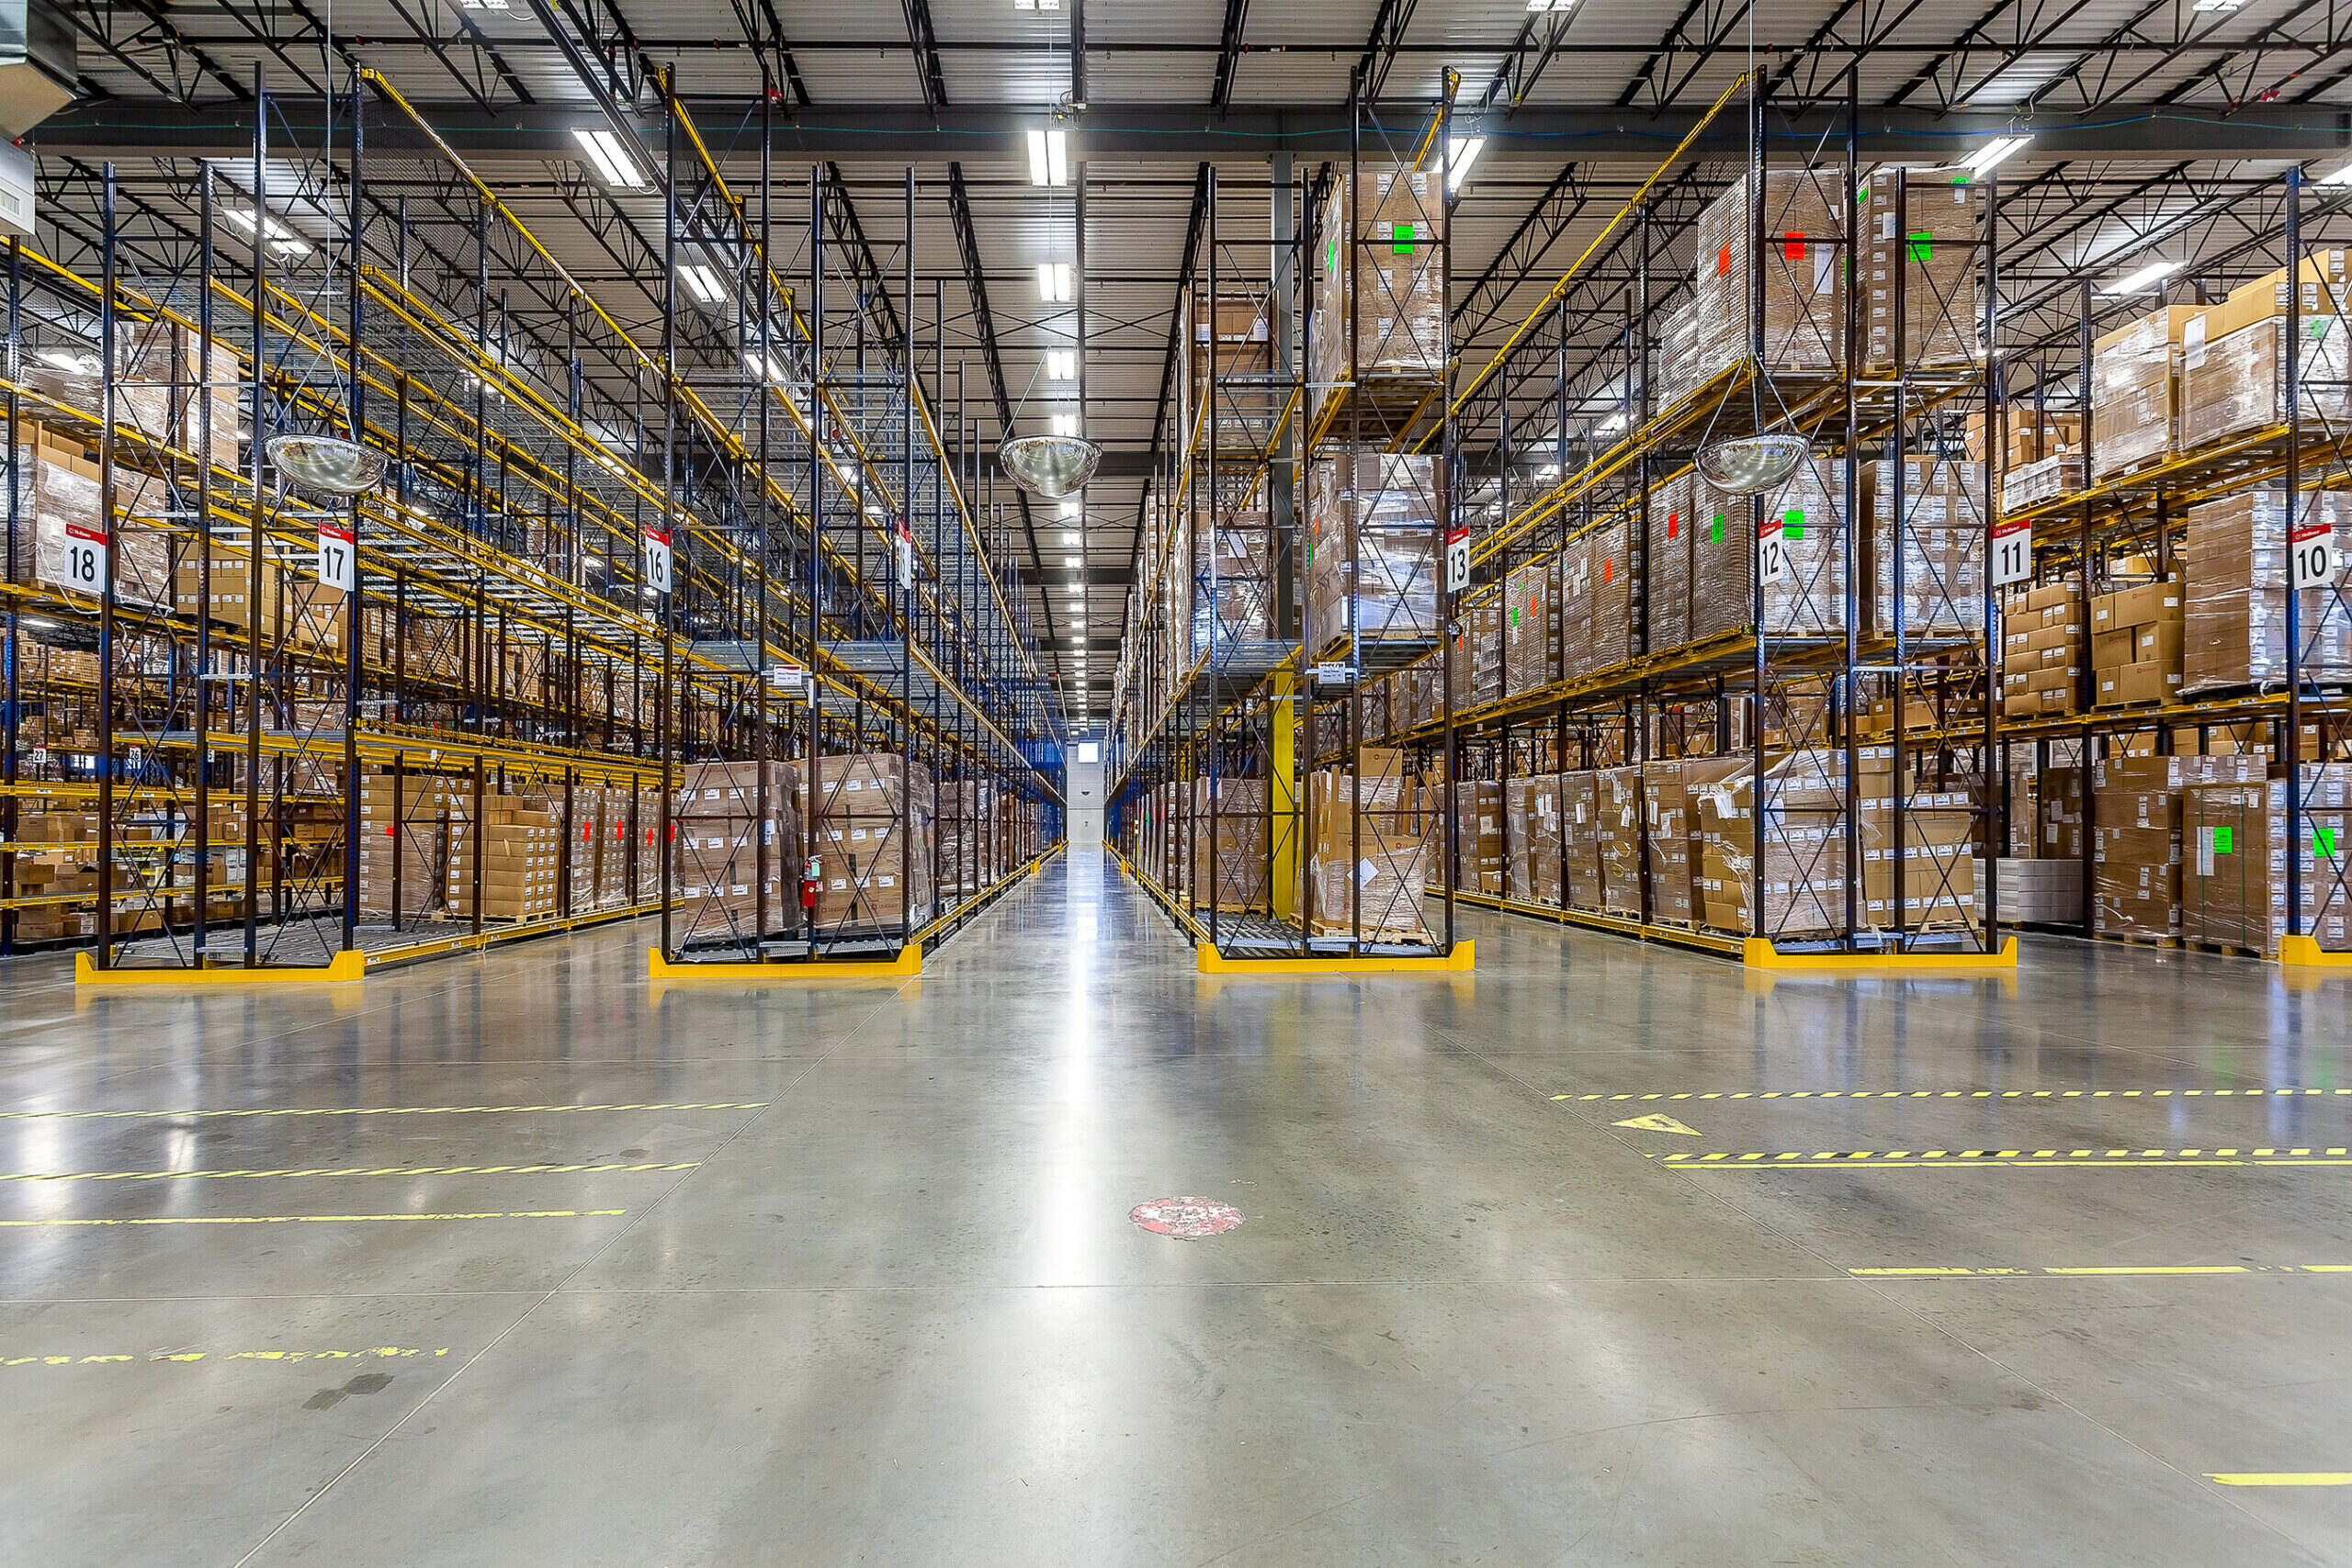
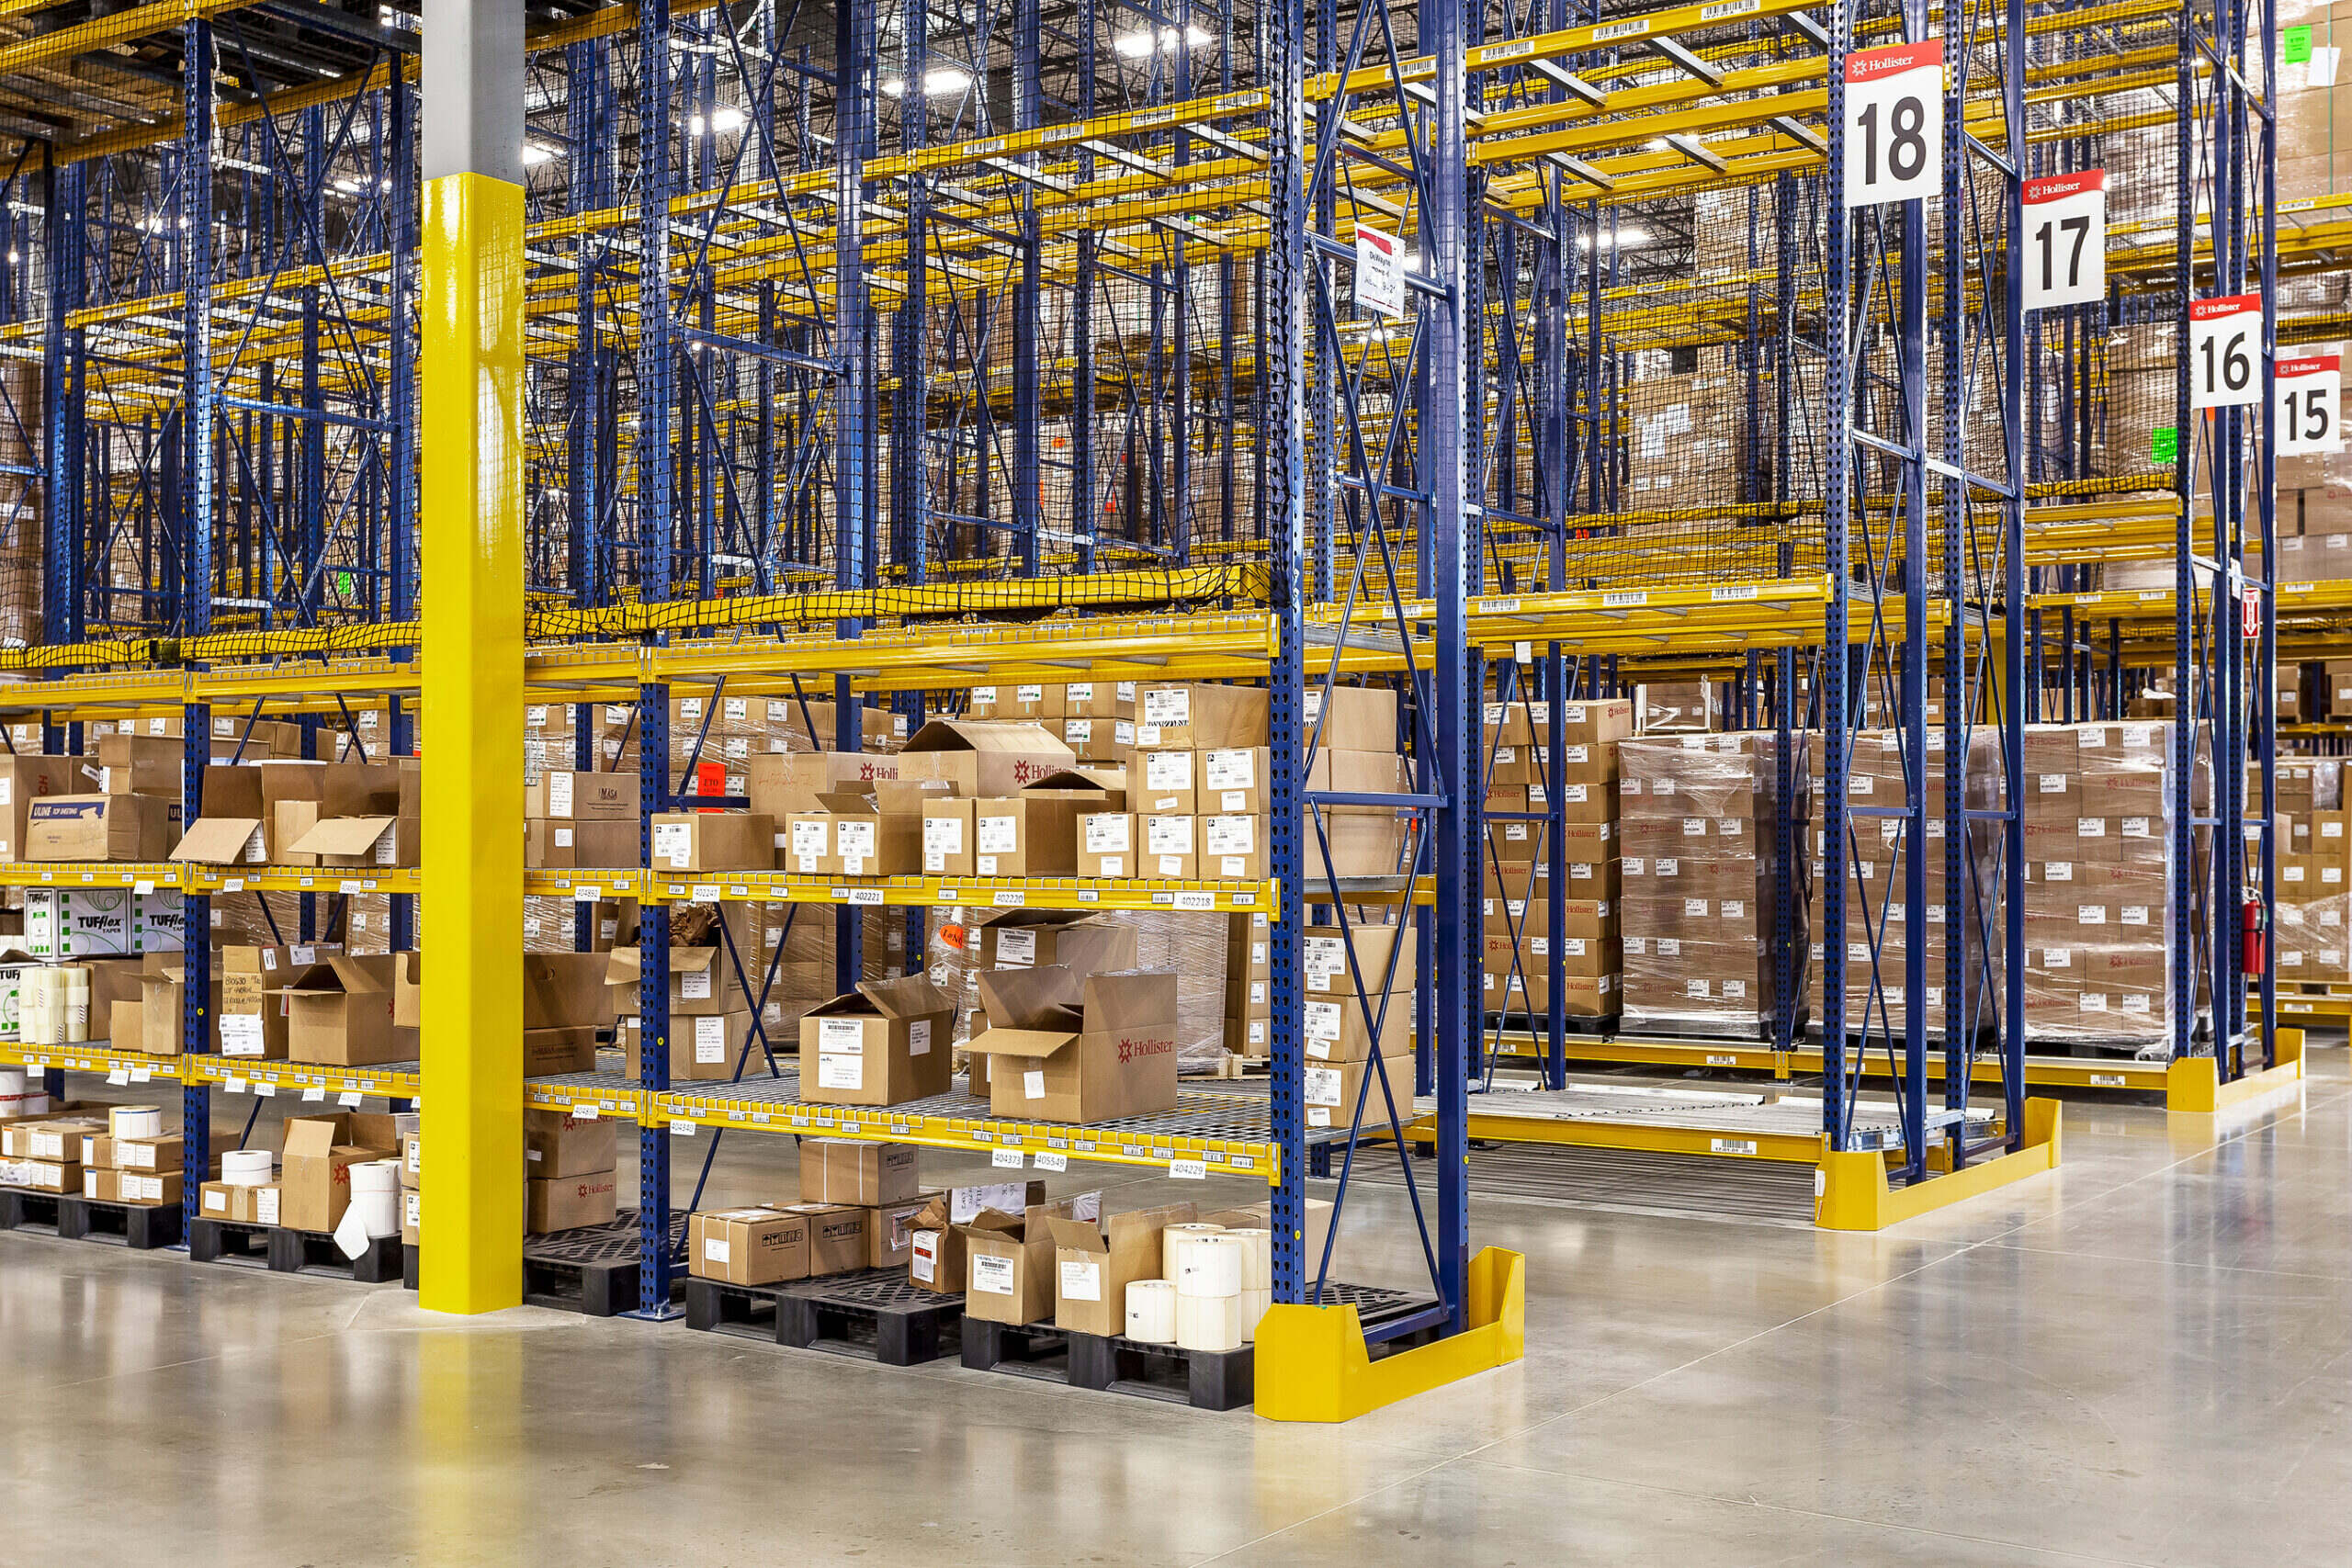
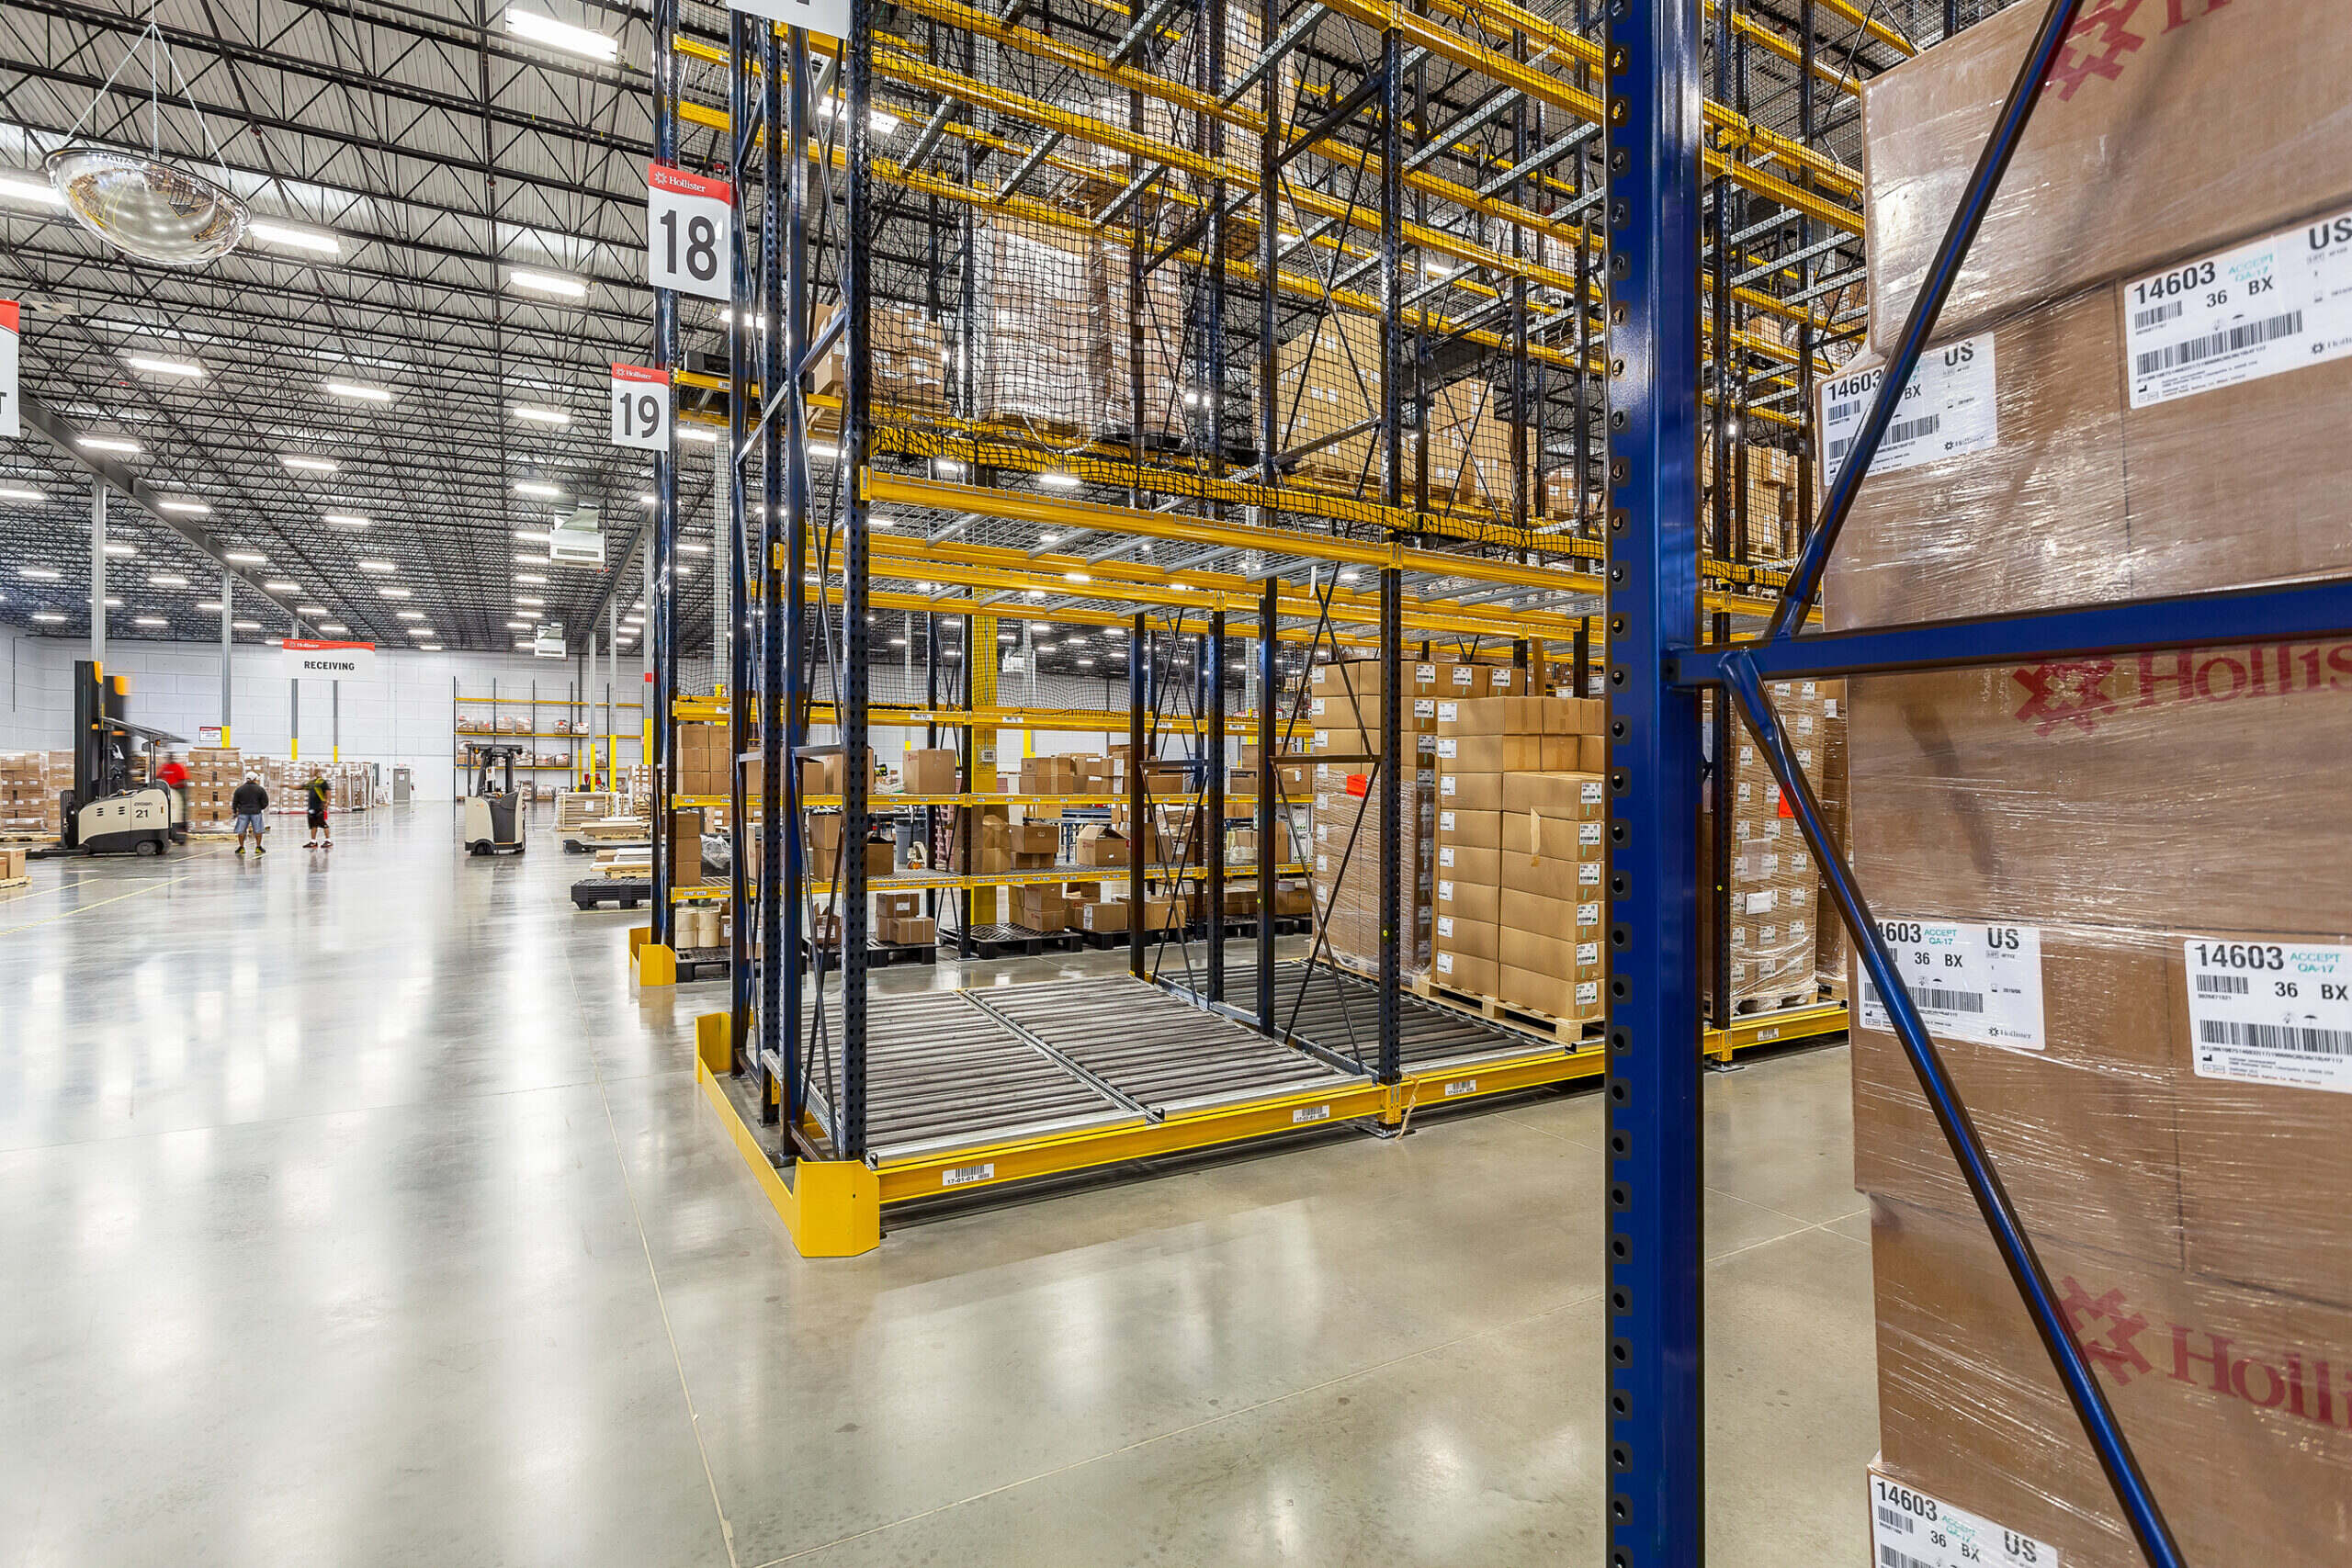
Our customer constructed a new 240,000 square-foot distribution center to facilitate continued growth and provide operational efficiency to increase service levels to their customers.
Customer Goals
Consolidate
storage of manufactured products.
Maximize
the entire space in their existing facility.
Find
the best solution for their needs.
Partner
with a company to complete the project from start to finish.
We designed a system that would fulfill their needs. Our team installed pick module including carton flow; pallet flow & shelving, selective rack, pallet flow rack, shelving, mezzanine, and rack safety netting.
The Results
Weaver Popcorn expanded its existing drive-in storage system, gaining over 3200 pallet positions and eliminating costly off-site storage fees. Our team also installed backstop netting to protect walking paths, as well as a combination of angle iron and guardrail to protect the newly installed rack.
17,200'+
Angle Iron
8,100'+
Custom Rub Rail
3,200+
Pallet Positions
200'
Safety Guard Rail
2500
Square Feet Of Safety Netting
Final Thoughts
At Storage Solutions, we pride ourselves in our ability to guide our clients throughout their project life cycle as trusted partners. By leveraging our strong partner relationships and extensive internal experience, we can develop an array of solutions to fit your unique facility needs, budget, and timeline.
Let us walk alongside you to identify the best possible solution to optimize your facility and ensure your next project runs smoothly.